


News
- Automatic H type chicken cages integrate tiered layer housing with mechanized feeding, egg collection, manure removal, and environmental control for commercial production requiring coordinated equipment, with configurations reaching 12 tiers and supporting large flock capacities.
Semi-automatic H type chicken cages combine mechanical feeding and drinking with selected manual procedures, providing practical equipment allocation for farms developing from approximately 1,000 to 10,000 layers while retaining operational flexibility.
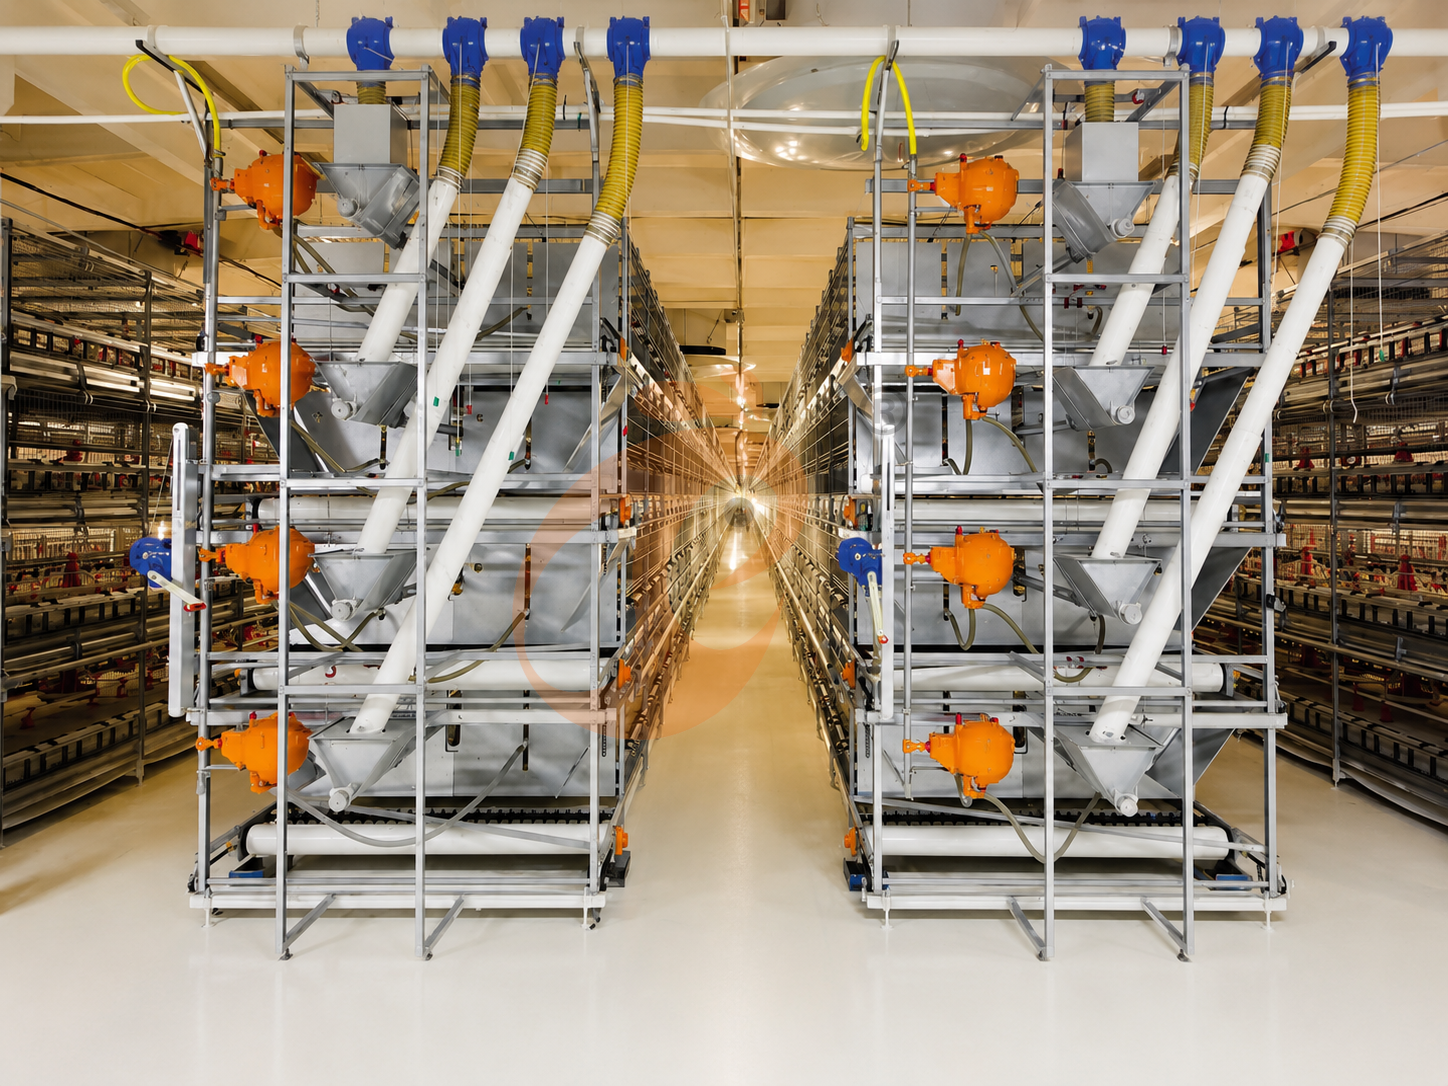
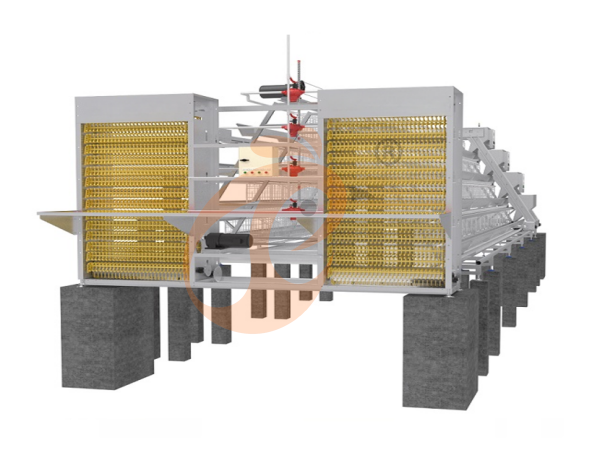
An H type layer cage system connects cage structure, feed delivery, water supply, egg transportation, manure handling, ventilation, and electrical control into one engineered poultry production arrangement.
Project selection depends on flock capacity, house geometry, equipment routing, labor organization, electrical infrastructure, maintenance access, and planned expansion rather than equipment purchase price alone.
- Correct equipment configuration improves vertical space utilization, material-flow consistency, operating organization, maintenance planning, and production continuity while establishing a technical foundation for future poultry-house development.
Get professional poultry farm construction guidance, equipment selection solutions, and the latest price lists, whatsApp to +8618830120193, click to learn more:
Start With The Farm, Not The Price
Choosing an H type chicken cage should begin with the production plan, not simply the equipment quotation.
Automatic H type chicken cages can support commercial projects where daily workflows require coordinated mechanical handling.
Semi-automatic H type chicken cages can suit projects where selected manual processes remain economically practical.
A commercial layer house may use 3–12 cage tiers, while a typical cage cell can be configured around 450 cm² per bird.
Data is for reference only.Swipe horizontally to view full table.
The critical question is how much work your farm must complete every day.
For example, a 100,000-layer project needs equipment that can maintain continuous material flow, while a smaller farm may benefit from retaining selected
manual operations.
A typical commercial house can be planned with 8–12 production rows, depending on building width and service-clearance requirements.
H Type Cage Turns Vertical Space Into Production Capacity
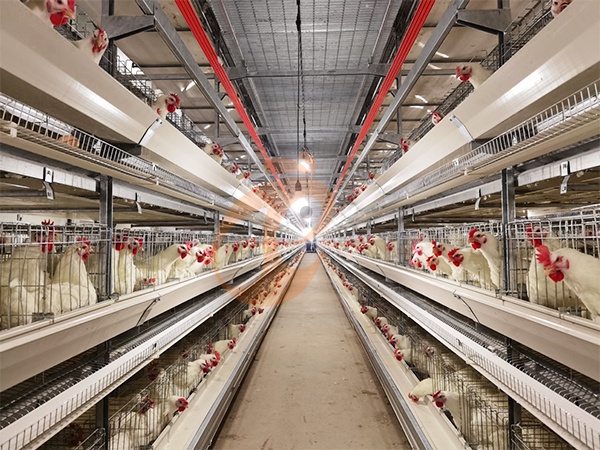
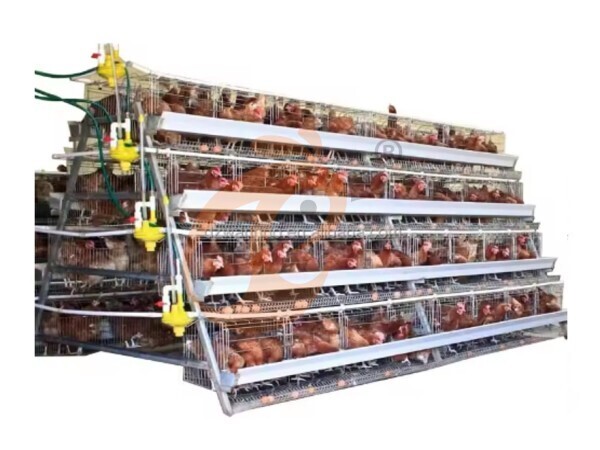
The H-frame configuration stacks cages vertically, allowing the farm to increase bird numbers without expanding the building footprint at the same rate.
Commercial H type layer cage systems are available in configurations reaching 12 tiers, depending on house structure and project requirements.
Data is for reference only.Swipe horizontally to view full table.
This vertical arrangement is particularly valuable when land is expensive or when the poultry house has a limited footprint.
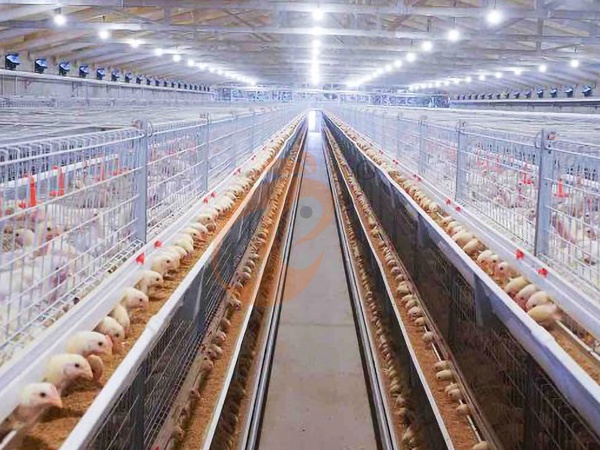
A properly engineered cage layout also creates defined routes for feed, water, eggs, and manure, while allowing inspection aisles to remain operational.
For structural planning, a cage row can be coordinated with a house clear height of approximately 4.5–11 m according to the selected tier configuration.
Automatic H Type: The Production Line Approach
Imagine the daily workflow: feed leaves the silo, travels through the feeding line, water reaches the nipples, eggs move toward the collection point, and manure is
transported outside the house.
Automatic H type chicken cages connect these separate processes into one operating system.
Data is for reference only.Swipe horizontally to view full table.
These figures show why automation becomes increasingly valuable as flock size grows.
The equipment is designed to keep material moving through the house with less dependence on repeated manual handling, while a properly synchronized drive
system can reduce unnecessary operating interruptions.
A complete automatic line can also be divided into multiple independently controlled zones, with individual drive sections commonly arranged at approximately
60–120 m intervals.
Semi-Automatic: Keep Control Where It Makes Business Sense
Semi-automatic H type chicken cages do not mean removing mechanical advantages.
A farm can automate repetitive processes such as feed distribution and drinking while keeping selected tasks under direct worker supervision.
Choose semi-automatic when:
→ Your flock size is relatively manageable.
→ Labor costs are acceptable in your region.
→ Your initial investment needs to remain controlled.
→ You want to upgrade gradually.
→ Your management team is comfortable with manual operations.
A semi-automatic configuration can also preserve practical access for routine inspection, with service aisles commonly planned around 1.0–1.5 m according to building layout.
The important point is that semi-automatic equipment should retain compatible interfaces for later system upgrades rather than becoming a closed configuration.
For manual inspection, cage access can be arranged around 0.6–0.9 m working clearance, depending on house width and equipment positioning.
Compare The Investment Through Operating Numbers
Do not compare automatic H type chicken cages and semi-automatic H type chicken cages only by equipment price.
Compare the technical workload each system is designed to handle, including installation complexity and the number of operating interfaces.
Data is for reference only.Swipe horizontally to view full table.
A common mistake is to compare only the purchase price.
For equipment investment, the better calculation is total cost of ownership.
A lower initial price can become less attractive if the system requires substantially more workers every day.
For farms operating for many years, automation may recover its additional investment through labor savings and higher management efficiency, while a properly
planned electrical cabinet can reserve 10–20% spare capacity for later expansion.
European union standard reference only.
The Decision Becomes Clearer With Farm Scale
A useful way to evaluate the H type layer cage system is to place the equipment against the actual flock size and house plan rather than using generic labels.
Data is for reference only.Swipe horizontally to view full table.
These capacity figures should be treated as project planning references rather than universal limits.
Cage quantity, bird density, house dimensions, ventilation design, and local production standards must be calculated before equipment is finalized.
For a commercial layer project, house modules can be divided into 30–60 m operating sections to simplify installation, inspection, and equipment maintenance.
Capacity Changes The Economics
Scenario A — Smaller Farm
A farm with a relatively small flock may not gain enough labor savings from complete automation to justify the additional investment.
Semi-automatic H type chicken cages can therefore offer a reasonable balance, particularly where daily egg volume remains within manageable manual handling limits.
Scenario B — Growing Farm
As flock numbers increase, repetitive manual work increases rapidly.
Automatic H type chicken cages become increasingly valuable when production requires continuous feed, egg, and manure movement across multiple house sections.
Scenario C — Large Commercial Farm
At commercial scale, the question changes from ''Can we afford automation?'' to ''Can we afford not to automate?''
When thousands or tens of thousands of birds are managed, labor efficiency, system stability, and centralized control can have a major impact on profitability.
At a 90% laying rate, every 10,000 layers can produce approximately 9,000 eggs per day, making material-handling design increasingly important as capacity
rises.
Equipment Integration Is More Important Than A Single Machine
An H type layer cage system should not be evaluated independently from the rest of the poultry house.
Data is for reference only.Swipe horizontally to view full table.
Our approach to poultry equipment focuses on system integration.
Cage dimensions, tier configuration, feeding lines, drinking systems, egg conveyors, manure belts, ventilation, and environmental controllers should be matched
according to the actual farm layout.
This reduces compatibility problems and gives customers one coordinated equipment solution rather than a collection of unrelated products.
Water-line zoning can be divided into approximately 30–50 m sections, helping maintain stable pressure and simplify flushing during routine maintenance.
Automation Is Also About Egg Quality
Egg collection is one of the clearest differences between the two configurations.
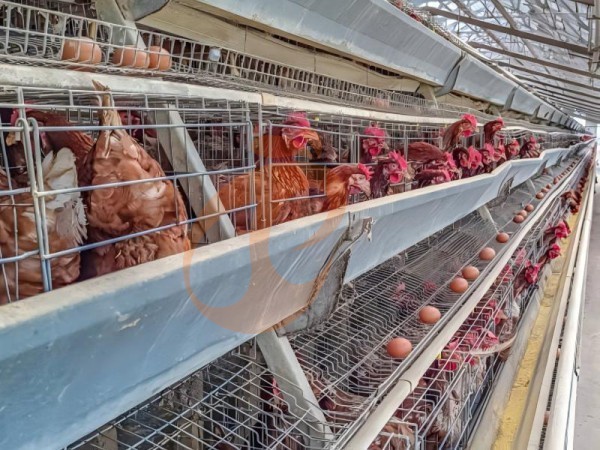
In an automatic system, eggs roll from the cage floor onto a conveyor and then move toward a central collection point.
Data is for reference only.Swipe horizontally to view full table.
A controlled transfer route reduces unnecessary handling between the cage and packing area.
For farms processing substantial daily egg volumes, this mechanical route can improve workflow consistency and reduce the number of manual transfer points, while belt alignment tolerance can be maintained within approximately 3 mm during installation.
Egg transfer routes can also be designed with a conveyor inclination of approximately 5–12°, depending on belt construction and the required transfer distance.
Manure Management Is A Separate Profitability Factor
Manure should not be treated as an afterthought.
A belt installed beneath each cage tier can transport manure toward the end of the poultry house, shortening the time waste remains beneath the birds.
Data is for reference only.Swipe horizontally to view full table.
A well-designed manure system can also support cleaner house management.
Automatic belt removal provides a predictable waste-removal route and can be integrated into the overall poultry-house workflow.
Manure transfer stations can be positioned approximately 1.5–3 m outside the main cage line to separate waste handling from routine bird inspection areas.
The Equipment Should Work As One System
The cage itself is only the structural core.
Feeding, drinking, ventilation, lighting, egg collection, manure removal, and electrical control must be coordinated around the cage layout.
Data is for reference only.Swipe horizontally to view full table.
This is where professional equipment engineering creates value.
A supplier should calculate the equipment configuration from house dimensions, flock capacity, climate conditions, electrical supply, and operating objectives rather than simply adding machines to a quotation.
For engineering coordination, cable routes can be separated from wet-cleaning areas by approximately 300 mm or more according to site conditions.
Ventilation control can also divide the poultry house into independently monitored zones, with sensor spacing commonly arranged around 30–50 m according to
building length.
Construction Quality Determines The Long-Term Equipment Value
A cage can look similar in a showroom while performing very differently after years of exposure to poultry-house humidity, manure, cleaning procedures, and mechanical loading.
Data is for reference only.Swipe horizontally to view full table.
For an equipment manufacturer, these specifications are not decorative product details.
They affect structural stability, corrosion resistance, component compatibility, and maintenance requirements throughout the service period, while cage alignment
during assembly can be controlled within approximately ±2 mm.
Fastener spacing can be maintained around 300–500 mm along selected structural connections, subject to the cage design and calculated loading requirements.
Automatic Or Semi-Automatic? Use The Engineering Scorecard
The choice becomes straightforward when the project is evaluated by measurable requirements instead of marketing labels.
Data is for reference only.Swipe horizontally to view full table.
The automatic option is particularly compelling when the farm needs centralized material handling and coordinated environmental management.
Semi-automatic equipment remains attractive where the project deliberately retains manual operations and uses automation only for selected production stages.
For a new poultry house, equipment positioning can be coordinated with structural columns at approximately 6–8 m spacing where the building design permits.
Build The Cage System Around Your Farm
The right H type chicken cage is ultimately a project-engineering decision.
A standard configuration may work for one poultry house but be unsuitable for another because building width, roof height, climate, flock size, and equipment routing are different.
Data is for reference only.Swipe horizontally to view full table.
Our H type chicken cage solutions are designed around the complete production line—not merely the cage body.
We can configure feeding, nipple drinking, egg collection, manure removal, ventilation, lighting, and control systems according to the farm layout and target capacity.
Whether starting with a semi-automatic project or building a fully automatic commercial layer farm, the objective remains the same: more organized production, measurable equipment performance, and a poultry system designed for long-term operation.
Frequently Asked Questions
Q1: What is the main difference between automatic and semi-automatic H type chicken cages?
Automatic H type chicken cages coordinate feeding, egg collection, manure removal, and related systems mechanically, while semi-automatic H type chicken cages retain selected manual procedures.
A complete automatic project can integrate multiple cage tiers and centralized material transfer, while semi-automatic layouts can isolate selected operations for manual handling.
Q2: Which H type cage system is better for a large layer farm?
Automatic H type chicken cages generally provide stronger operational scalability for large projects, especially when flock numbers exceed tens of thousands and repetitive labor becomes substantial.
For example, a 50,000-layer house producing around 45,000 eggs per day at a 90% laying rate creates a substantial daily handling requirement.
Q3: Can a semi-automatic H type cage system be upgraded later?
Yes, provided the original H type layer cage system includes compatible structural, electrical, and equipment interfaces, allowing selected automation modules to
be added during later expansion.
Planning approximately 10–20% spare electrical capacity and reserved equipment positions during the initial project can simplify future upgrades.
Taiyu (HK) Group - One Of China Biggest H Type Chicken Cages Manufacturer
H type chicken cages provide engineered multi-tier layer housing with coordinated interfaces for feeding, drinking, egg collection, manure handling, ventilation, and electrical control across commercial poultry projects.
Global factory-direct poultry equipment supply integrates cage production, mechanical systems, electrical coordination, installation guidance, technical documentation, and project-specific equipment configuration.
Turn-key engineering supports farm layout planning, equipment selection, manufacturing, shipment coordination, installation assistance, commissioning, and operational handover according to defined project parameters.
Poultry equipment packages can be configured for developing farms, commercial layer operations, and multi-house production facilities requiring coordinated mechanical and electrical systems.
Technical specifications, component selection, structural dimensions, equipment routing, and project documentation are coordinated with site conditions to establish a complete engineering delivery solution.
Contact Us To Received Your Customized Poultry Farm Plan
Headquarters And Branchs
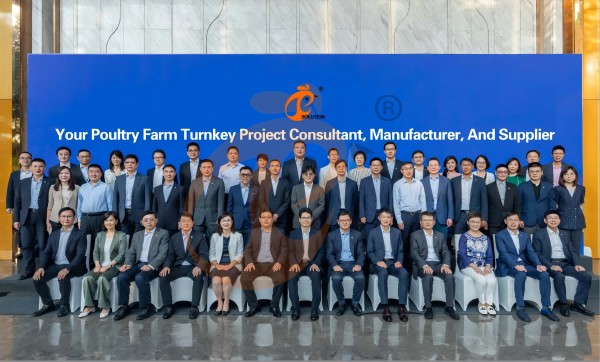
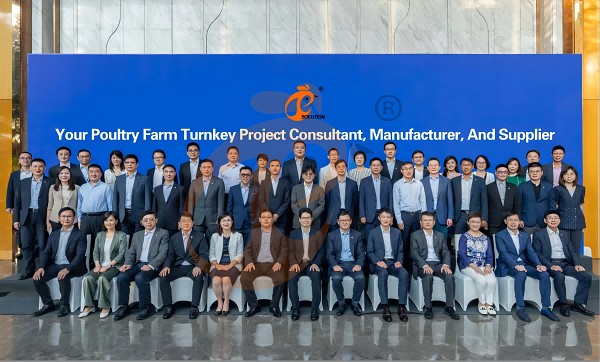
Hong Kong Headquarter Management Team
Hong Kong Headquarter Taiyu Industrial Group CO., LTD
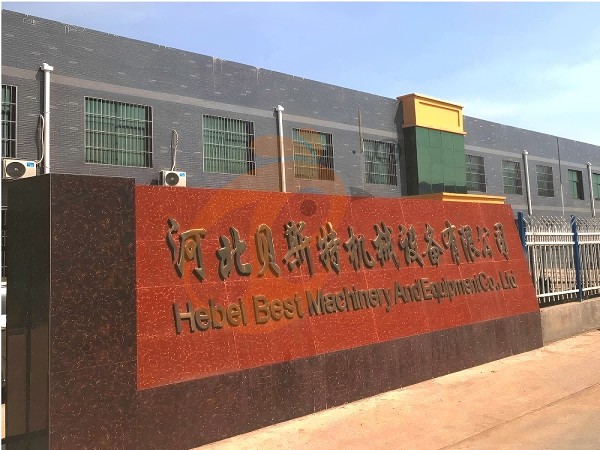
China Hebei Best Machinery And Equipment CO., LTD
Nigeria Vanke Machinery And Equipment CO., LTD
Tanzania Best Machinery And Equipment CO., LTD
Ethiopia Best Hebei Machinery Manufacturing PLC
Reception /24 WhatsApp NO. : +8618830120193
FAQ
How To Manage Lighting Programs In H-Type Layer Cage Houses?
Ensure even light distribution
Promotes laying rhythm
Egg production rate: 90-98%
FCR 1.9–2.1
What Are The Cleaning Procedures For H-Type Battery Cage System?
Use environmentally safe disinfectants
Clean manure troughs
Reduce pathogen spread
Egg production rate: 90-98%
How To Expand H-Type Chicken Cage Farm Without Reducing Efficiency?
Maintain automated feeding and drinking systems
Ensure uniform ventilation and lighting
Farm capacity per house: 30,000 - 100,000+0 birds
Labor savings: 70-90%
Product Recommendations
 Imported Vs Local H Type Chicken Battery Cages: Which Offers Better Quality?1. H Type Chicken Battery Cage layouts require coordinated house dimensions
2. Multi-tier cage structures support organized commercial layer production
3. Automatic systems connect feeding, drinking, manure, and egg handling
4. Engineering drawings define interfaces before equipment manufacturing begins
5. Reception /WhatsApp NO. : +8618830120193Read more A Type Battery Cage For Layers Vs Broilers: Which System Is More Suitable?1. A Type Battery Cage requires coordinated structural and utility planning
2. Layer housing layouts determine equipment positioning and service access
3. Automatic feeding reduces repetitive manual feed distribution work
4. Manure handling requires suitable conveyor or scraper interfaces
5. Reception /WhatsApp NO. : +8618830120193Read more 5 Practical Methods To Reduce Noise From Pralson Feeders1. Pralson feeders connect feed delivery with mechanical alignment requirements
2. Poultry houses require coordinated suspension and drive arrangements
3. Noise inspection should follow measurable mechanical checkpoints
4. Feeding performance depends on compatible component configuration
5. Reception /WhatsApp NO. : +8618830120193Read more Deep Litter System For Broiler Chickens | 7 Daily Checks1. Deep litter management depends on coordinated ventilation and drinking equipment
2. Daily inspections connect measurable house conditions with equipment operation
3. Feeding, water, airflow, and automation should follow synchronized procedures
4. Equipment specifications should match building dimensions and flock capacity
5. Reception /WhatsApp NO. : +8618830120193Read more Free Range System For Broiler Chickens | 7 Daily Management Checks1. Free-range houses require coordinated feed and water distribution systems with defined equipment layouts
2. Ventilation settings should reflect outdoor temperature and house dimensions through controller-based adjustments
3. Automatic doors require reliable scheduling and mechanical inspection procedures for consistent daily access
4. Daily records support preventive maintenance and equipment troubleshooting across interconnected farm systems
5. Reception /WhatsApp NO. : +8618830120193Read more Standard Vs Custom Broiler Chicken Cage Systems | Which Fits Your Farm?1. Standard cage systems use established component dimensions for conventional poultry houses.
2. Custom cage systems adapt equipment arrangements to actual building geometry and operating requirements.
3. Feeding and drinking equipment should be coordinated with cage placement during engineering.
4. Manure removal equipment should be planned before final equipment installation.
5. Reception /WhatsApp NO. : +8618830120193Read more Broiler Chicken Cage For Sale | 5 Key Factors Buyers Must Check1. Cage layouts require accurate building dimensions before equipment configuration begins
2. Feeding circuits should align with row lengths and service passages
3. Water systems need filtration and pressure control before commissioning
4. Manure conveyors require accessible inspection points for routine maintenance
5. Reception /WhatsApp NO. : +8618830120193Read more Nipple Drinker With Cup Vs Without Cup | Which Reduces Spillage?1. Nipple systems maintain consistent water access during poultry production stages
2. Cup designs help manage moisture around drinking locations effectively
3. Farm layouts influence equipment selection and installation methods
4. Different bird categories require suitable drinking system configurations
5. Reception /WhatsApp NO. : +8618830120193Read more Pellet Machine Energy Saving | 6 Effective Techniques1. Pelletizing efficiency depends on coordinated material preparation and conditioning
2. Stable feeding reduces unnecessary load fluctuations during production
3. Die and roller maintenance supports consistent mechanical compression
4. Cooling and screening protect finished pellet quality after compression
5. Reception /WhatsApp NO. : +8618830120193Read more Deep Litter Broiler System Investment Guide | 5 Decision Tips1. Deep litter housing requires accurate equipment positioning before installation
2. Ventilation calculations should match house volume and climate conditions
3. Feeding lines require progressive height adjustment during bird growth
4. Water systems need filtration and pressure control for stable delivery
5. Reception /WhatsApp NO. : +8618830120193Read more Free Range Broiler System Investment Guide | 5 Decision Tips1. Free-range broiler housing requires coordinated indoor production management
2. Automatic feeding reduces routine manual feed distribution work
3. Ventilation design depends on house volume and climate
4. Nipple drinking requires controlled pressure and regular inspection
5. Reception /WhatsApp NO. : +8618830120193Read more Floor Rearing Broiler Farming Profit | 6 Key Factors Explained1. Floor rearing systems require coordinated airflow and feeding equipment
2. Broiler houses need consistent water access throughout cycles
3. Environmental sensors provide measurable operating conditions for controllers
4. Maintenance schedules help prevent equipment-related production interruptions
5. Reception /WhatsApp NO. : +8618830120193Read more Turnkey Poultry Equipment Investment | 5 Practical Decision Tips1. Commercial poultry layouts require coordinated equipment positioning
2. Ventilation calculations should precede final equipment quantities
3. Feeding systems require compatible electrical and mechanical interfaces
4. Climate conditions influence cooling and airflow configuration
5. Reception /WhatsApp NO. : +8618830120193Read more Battery Cage For Layers ROI | 5 Practical Profit Analysis Tips1. Battery Cage For Layers layouts require coordinated structural and ventilation calculations
2. Layer cage system dimensions should match building geometry and service access
3. Automatic layer cage system integration depends on compatible mechanical and electrical interfaces
4. Commercial poultry equipment planning should separate capital costs from recurring operating expenses
5. Reception /WhatsApp NO. : +8618830120193Read more Broiler Chicken Cage ROI | 5 Practical Profit Analysis Tips For Investors1. Broiler Chicken Cage layouts depend on actual building dimensions and structure
2. Feed system sizing should follow required production throughput calculations
3. Ventilation specifications should reflect house volume and climate conditions
4. Manure equipment selection should consider line length and drive capacity
5. Reception /WhatsApp NO. : +8618830120193Read more 7 Ways To Prevent Pellet Machine Blockages Quickly1. Pellet machines convert prepared feed into uniform compact pellets
2. Stable feeding supports consistent compression throughout production
3. Conditioning improves material flow before pelletizing begins
4. Die selection connects formulation requirements with pellet dimensions
5. Reception /WhatsApp NO. : +8618830120193Read more A Type Poultry Cage Vs Floor Rearing System: 5 Performance Comparisons1. A Type poultry cage layouts determine equipment positions and maintenance access
2. Feed distribution requires coordinated drive systems and suitable delivery routes
3. Manure removal depends on belt dimensions, motor selection, and discharge planning
4. Environmental controls connect sensors, ventilation equipment, and house conditions
5. Reception /WhatsApp NO. : +8618830120193Read more Poultry Equipment Supplier | 5 Practical Tips To Choose The Right One1. Poultry equipment selection depends on house dimensions and flock capacity
2. Ventilation planning should account for climate and building structure
3. Feeding systems require coordinated capacity calculations before installation
4. Water systems require filtration and pressure checks before commissioning
5. Reception /WhatsApp NO. : +8618830120193Read more Battery Cage For Layers Cost | 6 Key Factors Affecting Price1. Layer cages organize birds vertically within dedicated housing rows
2. Feeding systems distribute feed consistently across cage sections
3. Manure equipment transfers waste toward designated collection areas
4. Water systems regulate drinking supply throughout production rows
5. Reception /WhatsApp NO. : +8618830120193Read more Broiler Chicken Cage Cost | 6 Key Factors Affecting Price And Budget1. Broiler cage projects require coordinated structural and mechanical specifications
2. House dimensions determine cage rows and equipment placement
3. Feeding and drinking systems require compatible connection layouts
4. Environmental systems depend on ventilation and cooling requirements
5. Reception /WhatsApp NO. : +8618830120193Read more How To Maximize Water Efficiency With Nipple Drinkers | 6 Tips1. Nipple drinkers provide controlled water delivery for poultry
2. Pressure regulation supports stable drinking-line operation
3. Filtration helps protect internal nipple components
4. Scheduled flushing removes accumulated line contaminants
5. Reception /WhatsApp NO. : +8618830120193Read more How To Upgrade Pellet Machines | 6 Practical Strategies1. Pelletizing performance depends on coordinated material preparation and mechanical compression
2. Feed moisture and particle size directly influence forming stability
3. Cooling and screening determine finished-product handling characteristics
4. Equipment interfaces should be planned before installation begins
5. Reception /WhatsApp NO. : +8618830120193Read more Poultry Cage Cost Per Bird Vs Total Project Cost: 5 Smart Comparisons1. Poultry cage layouts require accurate building dimensions before equipment production
2. Cage capacity calculations depend on selected housing configuration and tiers
3. Equipment routes should maintain accessible maintenance and service clearance
4. Electrical specifications must match local power infrastructure and motors
5. Reception /WhatsApp NO. : +8618830120193Read more Which H Type Chicken Cage Design Is Best For 20,000+ Layer Poultry Farms?1. H type chicken cage layouts require accurate building dimensions for equipment coordination
2. Automatic feeding routes should align with cage rows and service passages
3. Manure systems require planned access for inspection and scheduled maintenance
4. Egg collection equipment should connect cage rows with central transfer points
5. Reception /WhatsApp NO. : +8618830120193Read more Is Deep Litter System Suitable For Broilers? | 5 Answers1. Proper poultry farming requires stable environmental control mechanisms
2. Modern equipment ensures high animal welfare standards
3. Quality management systems reduce disease risks significantly
4. Reliable automation optimizes feed conversion efficiency daily
5. Reception /WhatsApp NO. : +8618830120193Read more Is Free Range System Suitable For Broilers? | 5 Practical Answers1. Free range broiler houses combine indoor control with outdoor access
2. Feeding equipment maintains predictable daily feed distribution
3. Drinking systems support continuous access to clean water
4. Ventilation equipment manages changing indoor environmental conditions
5. Reception /WhatsApp NO. : +8618830120193Read more Floor Rearing System For Broiler Chickens | 5 Daily Management Checks1. Floor rearing systems require coordinated equipment layouts
2. Feeding lines should align with house dimensions and flock capacity
3. Water systems require filtration, regulation, distribution, and flushing
4. Ventilation systems depend on airflow calculations and building structure
5. Reception /WhatsApp NO. : +8618830120193Read more How To Reduce Operating Costs With Poultry Equipment | 6 Tips1. Feed distribution accuracy supports controlled material allocation across poultry houses
2. Environmental sensors provide continuous measurements for automated equipment adjustment
3. Water monitoring helps identify abnormal consumption and potential system leakage
4. Preventive inspection supports mechanical reliability throughout equipment operating cycles
5. Reception /WhatsApp NO. : +8618830120193Read more A Type Battery Cage Vs Cage-Free System: Which Is More Profitable For Layers?1. A Type Battery Cage layouts require accurate building dimensions before equipment quantities are calculated
2. Feeding systems should align drive capacity with planned row lengths
3. Egg conveyors require coordinated transfer heights between housing and packing areas
4. Manure systems should match belt length, discharge direction, and removal cycles
5. Reception /WhatsApp NO. : +8618830120193Read more Floor Rearing Broiler House Design | 6 Practical Layout Guidelines1. Floor plans should maintain unobstructed routes between production zones and equipment access points
2. Feeder suspension should allow adjustment throughout broiler growth cycles
3. Water pipelines require accessible filtration and pressure-control positions
4. Ventilation components should align with calculated airflow paths and house geometry
5. Reception /WhatsApp NO. : +8618830120193Read more Nipple Drinker System Design | 5 Key Planning Tips For Farms1. Nipple lines require coordinated hydraulic planning across pressure, filtration, flushing, and suspension components
2. Bird access depends on correct drinking-line positioning throughout each production stage
3. Water quality should be evaluated before finalizing filtration and treatment equipment
4. Pipeline design should provide practical access for inspection and routine cleaning
5. Reception /WhatsApp NO. : +8618830120193Read more 7 Ways To Reduce Maintenance Costs For Pralson Feeders1. Pralson Feeders maintenance depends on correct installation and scheduled inspection
2. Automatic feeding lines require coordinated mechanical and electrical checks
3. Feed residue management supports consistent equipment operating conditions
4. Component records simplify replacement planning across production cycles
5. Reception /WhatsApp NO. : +8618830120193Read more 6 Practical Tips To Reduce Maintenance Costs Of Nipple Drinkers1. Nipple drinkers maintain controlled water access for poultry
2. Regular inspections prevent unnecessary mechanical service interruptions
3. Clean pipelines support stable equipment operation throughout production
4. Proper maintenance improves reliability across repeated flock cycles
5. Reception /WhatsApp NO. : +8618830120193Read more 5 Ways To Improve Pralson Feeder Reliability On Farms1. Pralson feeders distribute feed through coordinated mechanical systems
2. Regular inspections reduce unexpected operational interruptions significantly
3. Feed quality influences smooth equipment performance daily
4. Preventive maintenance supports stable production across cycles
5. Reception /WhatsApp NO. : +8618830120193Read more What Are The Installation Requirements For An A Type Battery Cage System? 6 Clear Guidelines1. Building dimensions determine the final cage-row arrangement and equipment positioning
2. Structural preparation provides the foundation for accurate cage assembly and utility integration
3. Feeding, drinking, manure, and egg systems require coordinated installation sequencing
4. Commissioning records verify mechanical movement, electrical connections, and water delivery
5. Reception /WhatsApp NO. : +8618830120193Read more Energy Saving Tips For Pralson Feeders | 6 Effective Methods1. Automatic feeders require coordinated electrical and mechanical settings
2. Feed distribution should remain consistent across line sections
3. Routine inspection helps identify developing mechanical changes
4. Flock growth requires corresponding equipment adjustment
5. Reception /WhatsApp NO. : +8618830120193Read more Commercial Battery Cage For Layers Vs Small Farm Cage | Which Should You Choose?1. Commercial layer cage systems optimize bird housing through structured engineering designs
2. Multi-tier cage layouts improve poultry house utilization with controlled equipment placement
3. Feeding systems support accurate nutrition delivery across commercial production areas
4. Manure management equipment maintains cleaner operational environments inside chicken houses
5. Reception /WhatsApp NO. : +8618830120193Read more Commercial Broiler Chicken Cage Vs Small Farm Cage | Which Should You Choose?1. Commercial broiler cages require accurate engineering calculations
2. Farm layouts influence equipment selection and production efficiency
3. Feeding systems connect with complete poultry management procedures
4. Cage structures support organized commercial farming processes
5. Reception /WhatsApp NO. : +8618830120193Read more Adjustable Vs Fixed Height Pralson Feeders | Which Reduces Waste?1. Adjustable feeders improve chicken house feeding management efficiency
2. Equipment structures support stable poultry production processes
3. Modern systems reduce unnecessary feed handling operations
4. Engineering designs improve farm operational consistency
5. Reception /WhatsApp NO. : +8618830120193Read more Electric Vs Diesel Pellet Machines | Which Saves More Energy?1. Electric pellet machines process feed materials efficiently
2. Diesel systems provide flexible operation options for farms
3. Energy selection influences poultry production efficiency
4. Feed processing requires stable equipment performance
5. Reception /WhatsApp NO. : +8618830120193Read more
Search
Hot product
 IoT Poultry Farming System1. CO₂ 0–5,000 ppm range
2. NH₃ 0–100 ppm
3. RH ±3%
4. Thresholds in the 10–25 ppm range
5. Reception /WhatsApp NO. : +8618830120193Read more Overall Structure IoT System In The Farm1. Breeding planning framework
2. CCTV
3. Poultry digital platform - comprehensive large screen
4. Alarm management
5. Reception /WhatsApp NO. : +8618830120193Read more Poultry House Environmental Control Smart IoT System1. Precision ventilation
2. Full site equipment control
3. Self diagnosis alarm system
4. European standard hardware
5. Reception /WhatsApp NO. : +8618830120193Read more
Contact us
Phone(whatsapp No. ):
E-mail:
Office 1 (Hong Kong):
Flat/RM A, 15/F, ManlyCommercial Building 15 Soy Street, Mong Kok
Office 2 (China Mainland):
Flat/RM 2416, 24/F, Runxing Building, Youyi Nan Street, Shijiazhuang City, Hebei Province