


News
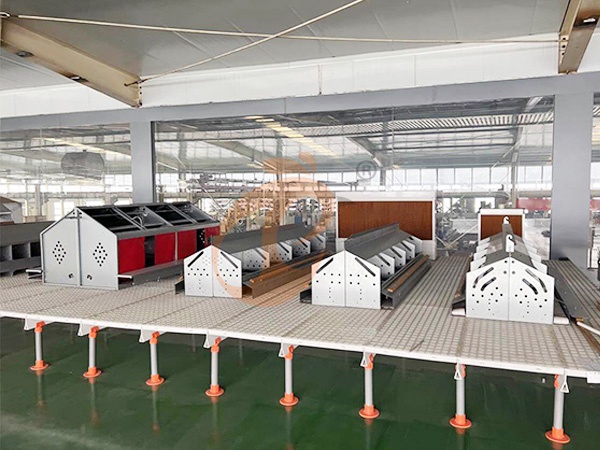
Floor rearing system integrates automated poultry equipment with flexible farm layouts, supporting 10,000 birds and 24-hour management cycles.
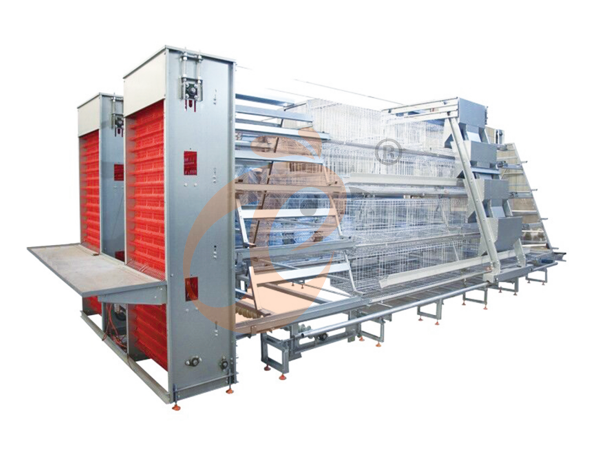
Cage system combines precision feeding and controlled production structures with 6-tier designs for commercial operations.
Cost comparison covers investment, operation, maintenance, and equipment selection strategies for modern farms.
Advanced chicken house equipment solutions improve workflow through sensors, motors, and environmental control units.
Professional engineering planning helps farms select suitable systems with 95% equipment matching accuracy.
Get professional poultry farm construction guidance, equipment selection solutions, and the latest price lists, whatsApp to +8618830120193, click to learn more:
Floor Rearing System Cost Analysis
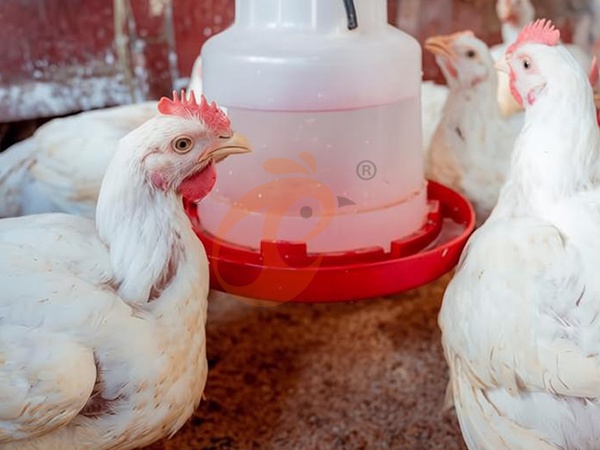
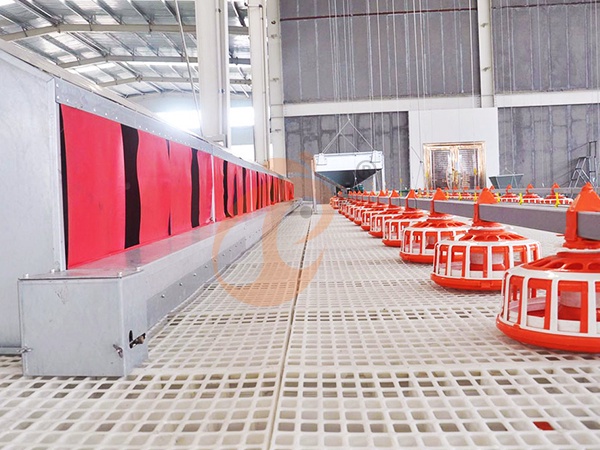
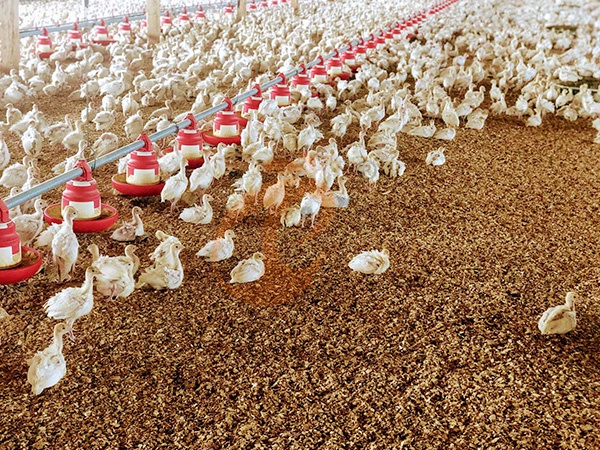
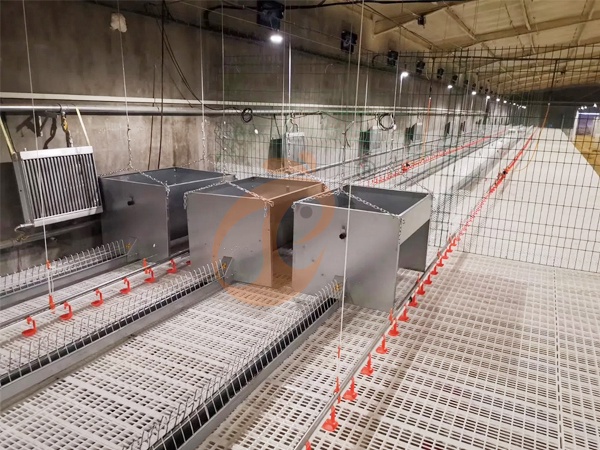
Floor rearing system focuses on open-house production management with integrated feeding, drinking, ventilation, and litter control equipment.
Commercial farms selecting a complete floor rearing poultry system usually evaluate construction requirements, equipment configuration, and operating return before installation.
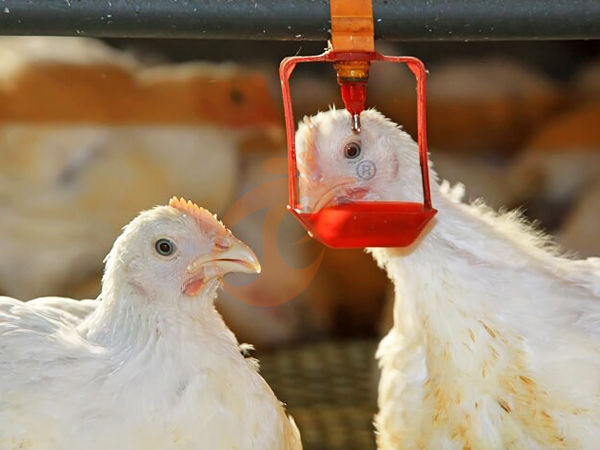
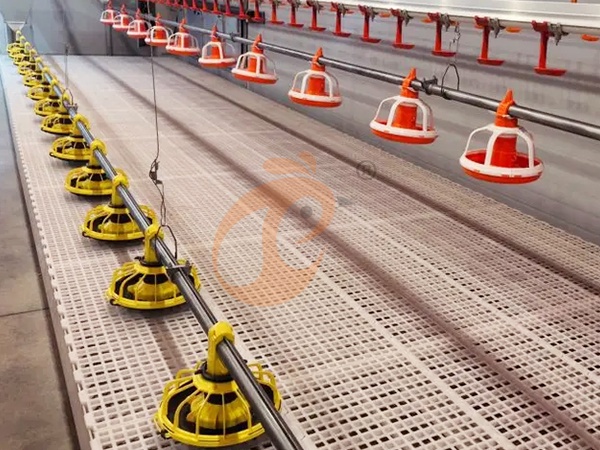
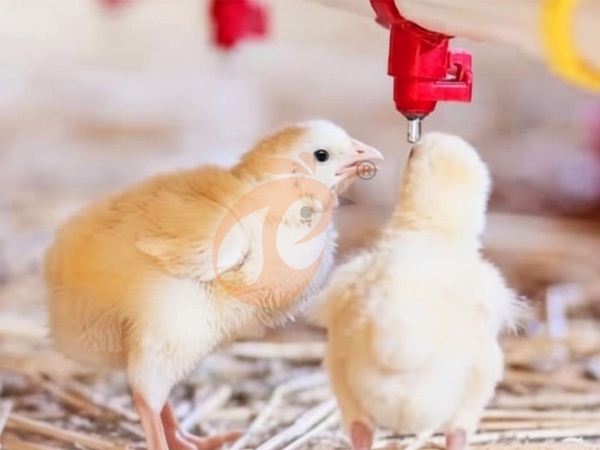
Modern suppliers provide automatic feeding lines, nipple drinking systems, climate controllers, and ventilation solutions to create complete poultry production environments.
A professional floor rearing layout can support flexible expansion with 120-meter house lengths and 18-hour daily equipment operation schedules.
Data is for reference only.Swipe horizontally to view full table.
Floor rearing equipment investment depends on house design, automation structure, and local construction conditions.
An engineered solution with galvanized components, 2.5mm material thickness, and modular assembly design can simplify installation procedures.
Cage System Equipment Configuration
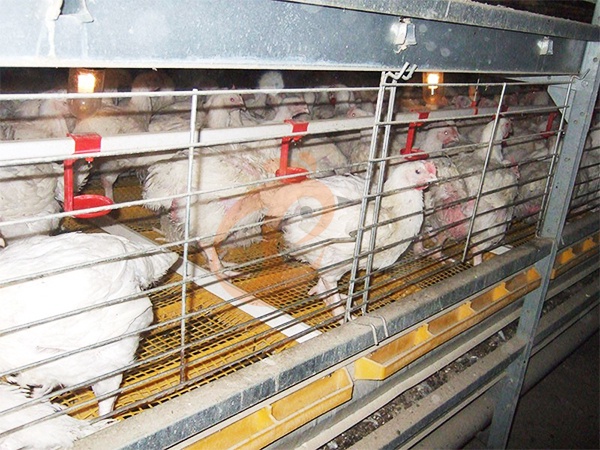
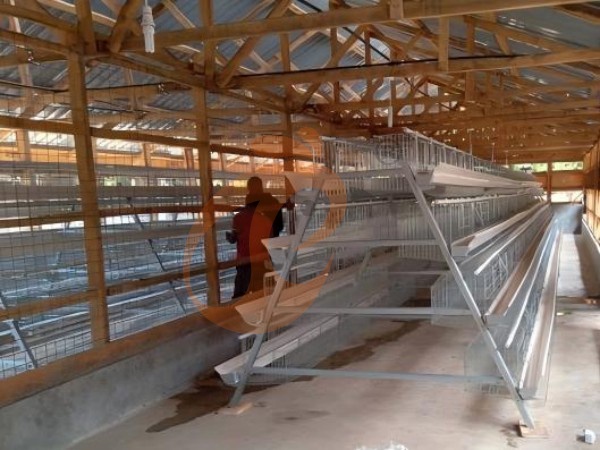
Cage system uses vertical space utilization combined with automated feeding, manure handling, and egg collection equipment.
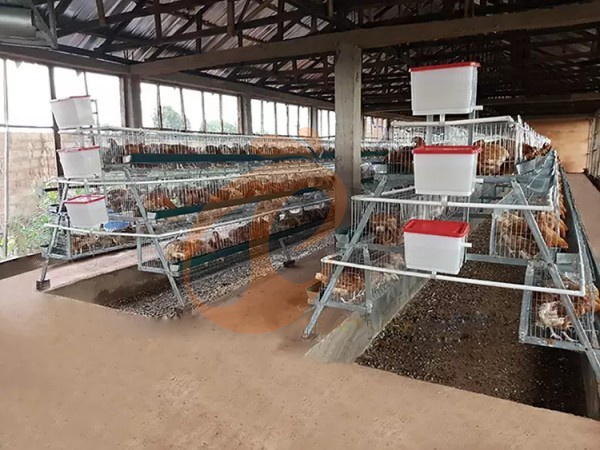
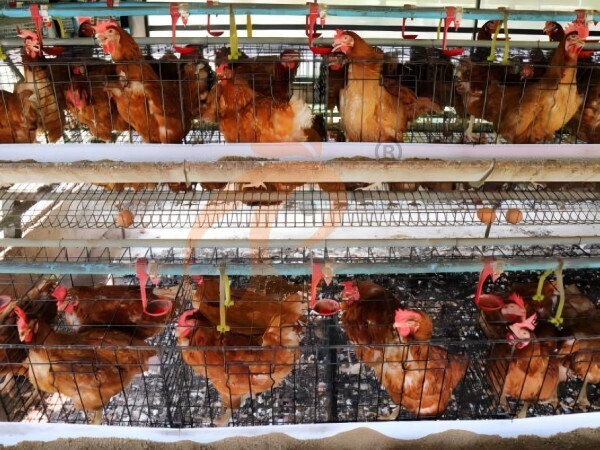
For layer farms, poultry cage equipment provides structured management through galvanized steel frames, feed conveyors, and centralized control systems.
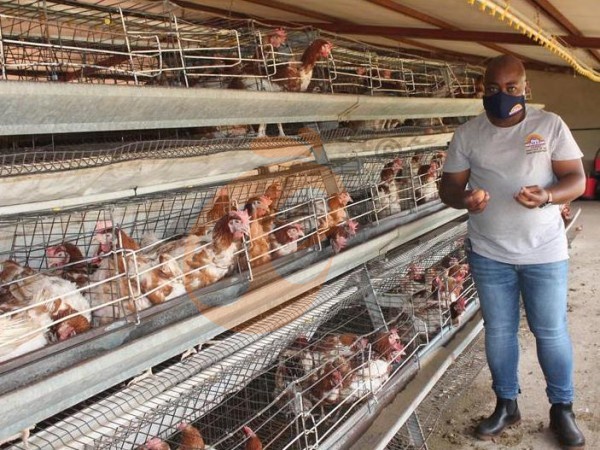
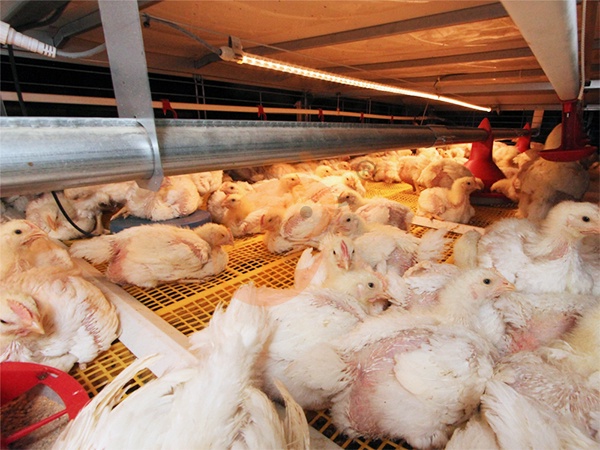
Battery cage projects commonly integrate multiple tiers, automatic auger feeding, and manure removal systems to improve operational organization.
A complete chicken cage system solution can include 8-row arrangements and 450-meter feed transmission distance for large-scale farms.
Data is for reference only.Swipe horizontally to view full table.
Cage system selection requires evaluation of bird capacity, equipment compatibility, and future production planning.
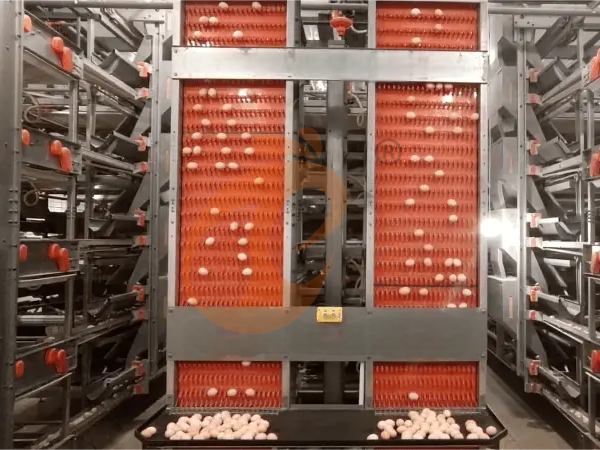
Automatic egg collection integration, with 98-meter conveyor sections and 30-minute cleaning cycles, improves daily management efficiency.
Investment Decision Model: Which System Fits Commercial Farms?
Choosing between floor and cage solutions requires analyzing business objectives rather than focusing on equipment purchase price alone.
Farm owners usually compare construction requirements, labor organization, energy consumption, and production targets before approving a project.
Floor rearing system supports farms requiring flexible housing structures, while cage system serves operations requiring intensive space utilization.
Engineering teams normally evaluate 15-year service expectations and 3-phase electrical compatibility before finalizing equipment specifications.
Data is for reference only.Swipe horizontally to view full table.
Equipment suppliers with turnkey capability can provide farm planning, production equipment, installation guidance, and after-sales support.
Poultry Equipment Selection Strategy
Engineering Perspective
Selecting poultry equipment requires matching mechanical design with production targets.
Automatic feeding equipment, drinking systems, and environmental controllers form the core infrastructure of commercial chicken houses.
A reliable supplier provides integrated solutions covering equipment manufacturing, installation supervision, and technical training.
System design normally considers airflow direction, feed distribution accuracy, and maintenance accessibility.
A ventilation fan configuration with 1400mm diameter blades and 38000m³/hour airflow capacity can support stable internal conditions.
Data is for reference only.Swipe horizontally to view full table.
Professional poultry equipment manufacturers design systems according to farm capacity, climate environment, and operation requirements.
Cost Efficiency Comparison Through Operation Analysis
A commercial farm evaluates cost efficiency through equipment lifespan, labor arrangement, and production consistency.
Floor systems generally require different management methods compared with cage installations because litter handling and bird movement patterns affect daily procedures.
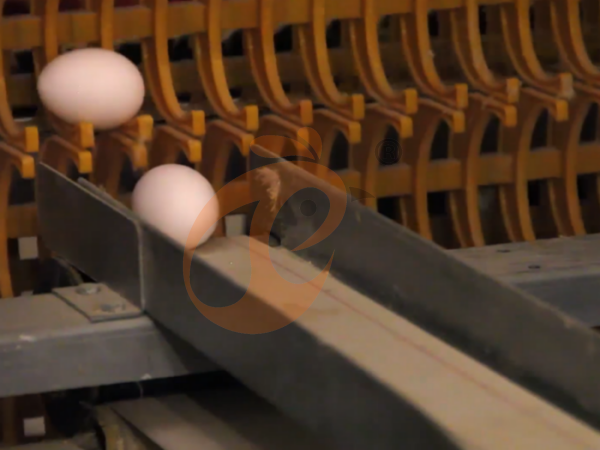
Cage systems integrate more mechanical components, including egg collection, manure transport, and automated feed delivery structures.
European union standard reference only.
Data is for reference only.Swipe horizontally to view full table.
Long-term profitability depends on project design quality, equipment durability, and farm management capability.
Advanced chicken house equipment with optimized components can reduce operational pressure through automated workflows.
Farm Automation And Future Development
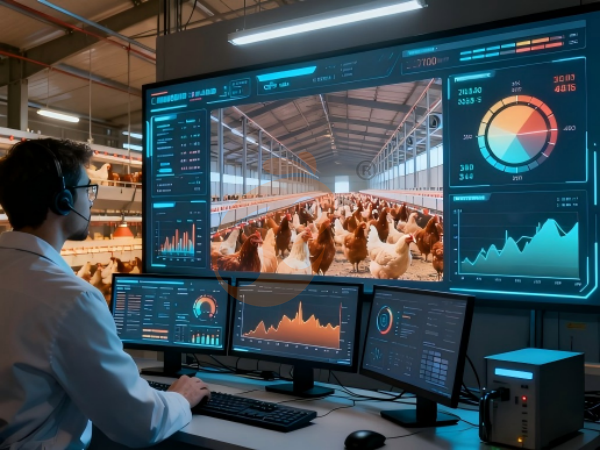
Modern poultry production is moving toward intelligent management with digital monitoring and automated control.
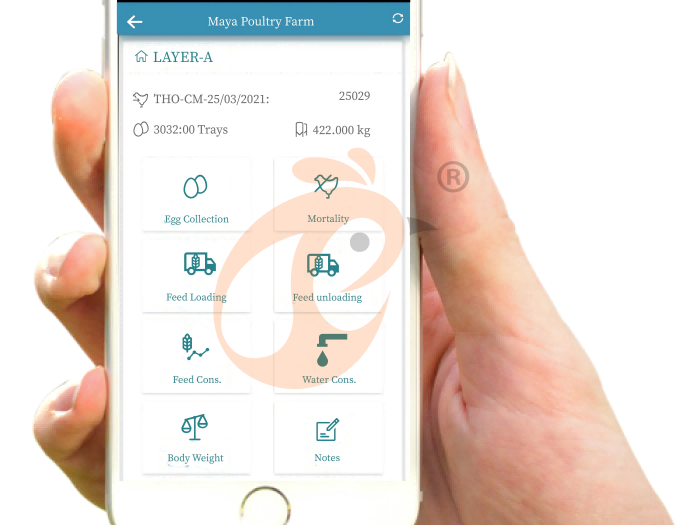
The combination of sensors, controllers, and mechanical systems allows farms to collect operational data during daily production.
A complete Turn-key poultry project can connect feeding, ventilation, lighting, and environmental monitoring into one management platform.
Intelligent poultry equipment solutions support farms requiring scalable production models with 24/7 monitoring capability.
Data is for reference only.Swipe horizontally to view full table.
Equipment Integration Value For Commercial Farms
Project Planning View
Commercial poultry farms require a complete equipment ecosystem rather than individual machines.
A professional poultry equipment supplier evaluates feeding capacity, ventilation balance, and automation compatibility before manufacturing.
Floor rearing system projects normally combine automatic feeders, drinking lines, ventilation fans, and environmental controllers into one coordinated structure.
Cage system projects integrate cage frames, egg collection conveyors, manure belts, and control cabinets for standardized operation.
Engineering teams usually review power requirements, building dimensions, and service access points before equipment production.
A customized design with 380V electrical configuration and 45-minute emergency response settings improves project reliability.
Data is for reference only.Swipe horizontally to view full table.
Floor Rearing System Vs Cage System: Marketing And Technical Balance
Market Application Analysis
Modern farms select production systems according to market demand, investment structure, and automation expectations.
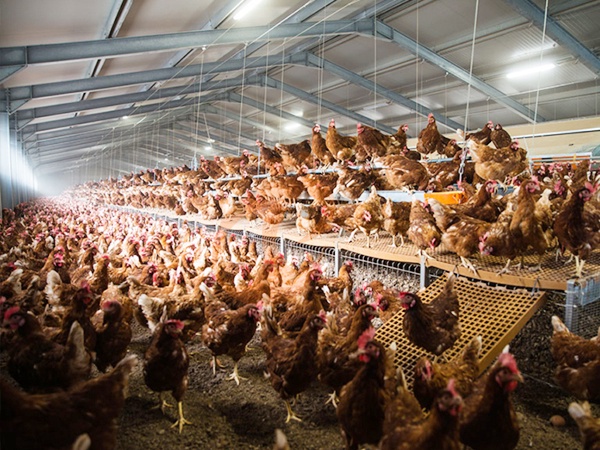
Floor rearing system provides an adaptable platform for farms requiring litter management and open housing concepts.
Cage system offers integrated mechanical operation through automatic feeding, egg collection, and manure removal technologies.
A complete poultry farm solution from a professional manufacturer connects equipment selection with long-term production planning.
Projects with 5000 to 50000 birds often require different equipment combinations because management targets vary significantly.
A supplier offering chicken house equipment packages can provide layout design, manufacturing, shipment, installation guidance, and technical support.
Professional Purchasing Guide For Poultry Investors
Decision Checklist Format
Commercial buyers can evaluate equipment selection through five technical checkpoints.
Production Scale
Farm capacity determines equipment quantity, building arrangement, and automation level.
Operation Model
Different management structures influence whether floor systems or cage systems create better workflow compatibility.
Maintenance Design
Equipment accessibility affects replacement procedures and daily inspection efficiency.
Expansion Capability
Modular systems allow future upgrades without replacing complete production lines.
Supplier Capability
Experienced manufacturers provide engineering drawings, production control, and installation support.
A complete Turn-key poultry project normally includes mechanical design, equipment manufacturing, installation supervision, and operator training.
Professional suppliers can configure systems with 240-meter feeding routes and 16 monitoring sensors for commercial requirements.
Technology Development Direction
Future Farming Scenario
The poultry industry is moving toward intelligent management through automation and digital monitoring.
Modern poultry equipment combines sensors, controllers, and mechanical components to improve production visibility.
Artificial intelligence monitoring, environmental data collection, and automated adjustment systems are becoming important parts of new farm designs.
Floor and cage systems are gradually adopting smart technologies to improve equipment coordination.
A future-ready chicken farm may include remote control platforms, automatic alarms, and data-based maintenance schedules.
Data is for reference only.Swipe horizontally to view full table.
Final Cost Evaluation Between Two Systems
Commercial Summary
The question of floor rearing system vs cage system depends on farm objectives, equipment requirements, and investment planning.
Floor solutions focus on flexible management with integrated feeding and environmental equipment.
Cage solutions focus on mechanical organization through structured production units.
Neither system can replace professional engineering analysis because every project has different construction conditions.
Selecting a manufacturer with complete poultry equipment capability helps reduce project risks during design, production, and installation stages.
A complete solution using automated chicken house equipment can support stable operation through 10-year equipment service planning and standardized spare parts supply.
Frequently Asked Questions
Q1: Which system requires more equipment integration for large farms?
Large farms usually require more automated modules because production scale may exceed 30000 birds and daily management becomes more complex.
Q2: Can floor rearing system include automatic equipment?
Yes, modern floor systems can include automatic feeding lines, nipple drinking systems, ventilation control, and environmental monitoring units with modular designs.
Q3: Why do farms compare cage system and floor system before investment?
Farm owners compare both systems because equipment structure, labor organization, construction requirements, and operational costs directly influence project return.
Taiyu (HK) Group - One Of China Largest Poultry Equipment Manufacturer
Poultry equipment provides integrated farm solutions covering automatic feeding systems, drinking systems, ventilation units, and environmental control equipment for commercial poultry projects.
Global factory direct supply supports international customers with standardized manufacturing processes, quality inspection procedures, and export documentation.
Professional poultry equipment engineering teams deliver Turn-key projects including layout planning, equipment production, installation guidance, and commissioning services.
Complete poultry equipment production lines support farms across different regions with customized solutions for various climate and production requirements.
Technical project management combines factory manufacturing capability with overseas service experience for efficient poultry farm construction.
Contact Us To Received Your Customized Poultry Farm Plan
Headquarters And Branchs
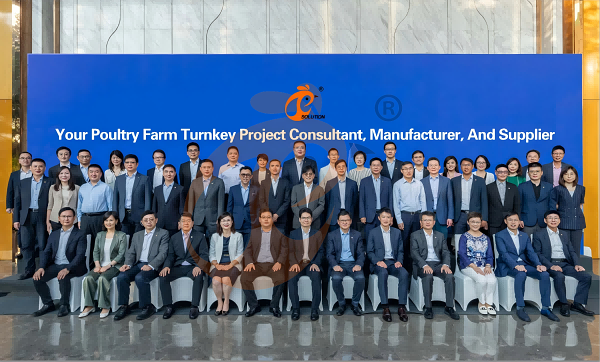
Hong Kong Headquarter Management Team
Hong Kong Headquarter Taiyu Industrial Group CO., LTD
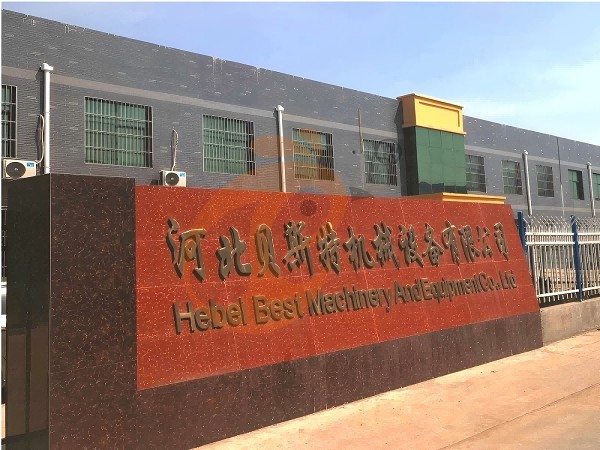
China Hebei Best Machinery And Equipment CO., LTD
Nigeria Vanke Machinery And Equipment CO., LTD
Tanzania Best Machinery And Equipment CO., LTD
Ethiopia Best Hebei Machinery Manufacturing PLC
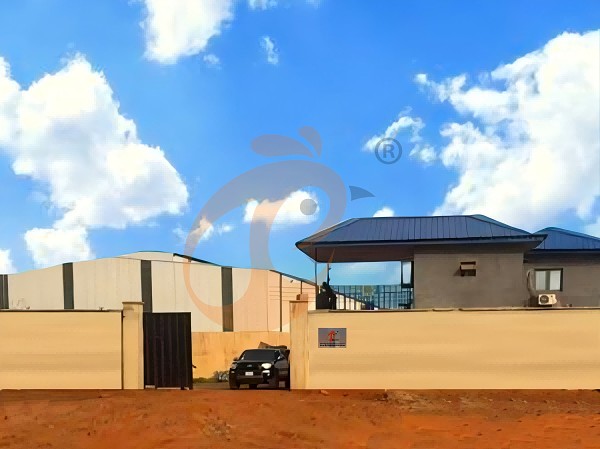
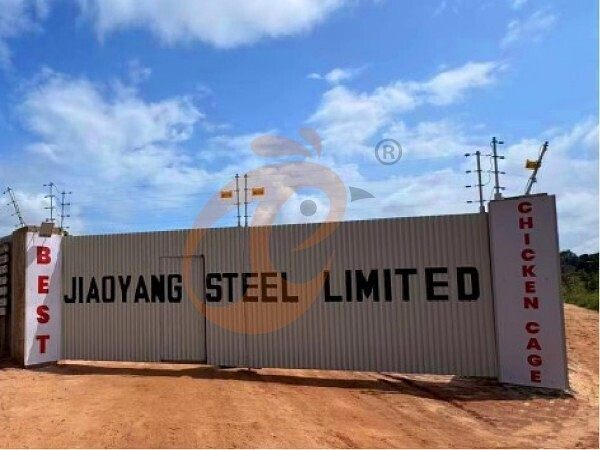
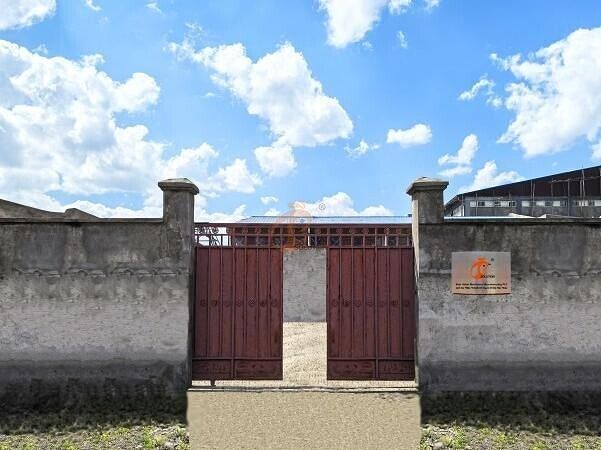
Reception /24 WhatsApp NO. : +8618830120193
FAQ
What Growth Performance Indicators Are Expected In Floor Rearing Poultry System?
Feed conversion ratio is maintained at 1.65–1.85 for commercial broilers.
Market slaughter age ranges from 38–45 days depending on breed selection.
What Disease Control Standards Apply In Floor Rearing Poultry System?
Flock vaccination coverage reaches 90%–98% depending on disease prevention program.
Pathogen reduction targets aim for 80%–90% decrease in bacterial load.
What Are The Manure Management Requirements In Floor Rearing Poultry System?
Ammonia emission control targets remain below 15 ppm through regular cleaning cycles.
Dry matter content is maintained above 65% to improve composting efficiency.
- poultry equipment
- automatic feeding system
- manure removal system
- chicken cage
- poultry farm
- poultry cage
- battery cage
- Layer cage
- automatic egg collection
- layer farm
- chicken farm
- chicken house
- chicken cage system
- poultry cage equipment
- modern poultry equipment
- poultry equipment manufacturers
- poultry equipment manufacturer
- poultry equipment supplier
- poultry equipment solutions
- poultry farm construction
- chicken house equipment
- automated chicken house
- egg collection conveyor
- egg collection equipment
- poultry equipment solution
- Tanzania
- Nigeria
Product Recommendations
 Pellet Machine Lubrication | 6 Essential Steps For Longevity1. Regular lubrication helps maintain mechanical contact surfaces during repeated pellet production cycles
2. Cleaning procedures reduce contamination around critical moving components during servicing operations
3. Inspection records provide measurable evidence for maintenance decisions across production periods
4. Correct lubricant selection supports bearings, gear systems, shafts, and transmission assemblies
5. Reception /WhatsApp NO. : +8618830120193Read more Manual Feeding Vs Feed Mixer Automation | Which Costs Less?1. Feed mixer automation connects preparation and distribution stages
2. Mechanical mixing reduces repeated manual feed handling
3. Controlled conveying establishes a fixed material route
4. Automatic feeding supports scheduled delivery operations
5. Reception /WhatsApp NO. : +8618830120193Read more Poultry Cage Price For Africa Vs Asia Market: 4 Cost Differences1. Poultry cage layouts depend on flock capacity and house geometry
2. Equipment specifications should align with local operating conditions
3. Shipping calculations require verified packing dimensions and quantities
4. Commissioning procedures should cover mechanical and electrical systems
5. Reception /WhatsApp NO. : +8618830120193Read more H Type Chicken Cages Vs Flat House Poultry Systems: Which Saves Space?1. H Type Chicken Cages distribute birds across multiple vertical levels
2. Automatic feeding equipment follows dedicated cage-row routes
3. Manure removal equipment transfers waste toward collection points
4. Building dimensions determine final equipment arrangement and capacity
5. Reception /WhatsApp NO. : +8618830120193Read more How To Avoid Common Buying Mistakes When Choosing An A Type Poultry Cage? 5 Smart Tips1. Cage selection should follow building dimensions and flock requirements
2. Equipment interfaces require verification before manufacturing starts
3. Technical drawings help prevent installation conflicts and modifications
4. Automation modules can be selected according to operational priorities
5. Reception /WhatsApp NO. : +8618830120193Read more How To Improve Growth Rate In Broiler Floor Rearing System | 5 Tips1. Broiler houses require coordinated airflow, feeding, and drinking equipment
2. Environmental conditions influence bird comfort and production consistency
3. Automatic systems reduce repetitive manual management during daily operations
4. Equipment layout should follow flock capacity and house dimensions
5. Reception /WhatsApp NO. : +8618830120193Read more Poultry Farm Equipment Cost | 6 Key Factors Affecting Price And ROI1. Poultry farm equipment selection should match bird capacity and building dimensions
2. Automatic systems coordinate repetitive operations across multiple production areas
3. Ventilation equipment requires airflow calculations based on house conditions
4. Lifecycle costing should include maintenance, energy, and replacement requirements
5. Reception /WhatsApp NO. : +8618830120193Read more Hot-Dip Galvanized Vs Painted Battery Cage For Layers | Which Lasts Longer?1. Hot-dip galvanization creates zinc-based protection around prepared steel surfaces
2. Layer-house humidity and ammonia influence corrosion exposure during operation
3. Automatic feeding and manure systems require compatible cage-bank layouts
4. Maintenance planning remains important throughout commercial equipment service
5. Reception /WhatsApp NO. : +8618830120193Read more High Density Vs Low Density Broiler Chicken Cages | Which Performs Better?1. Multi-tier cage structures organize commercial broiler production vertically
2. Automatic feeding reduces repetitive manual feed distribution work
3. Ventilation design must match total building heat loads
4. Manure removal equipment supports cleaner production workflows
5. Reception /WhatsApp NO. : +8618830120193Read more How To Upgrade Old Water Lines To Nipple Drinkers | 5 Steps1. Drinking lines require systematic inspection before replacement work begins
2. Nipple positions should follow bird access and house geometry
3. Pressure checks verify proper operation across complete lines
4. Flushing removes installation debris before flock commissioning
5. Reception /WhatsApp NO. : +8618830120193Read more Floor Rearing System For Broilers Vs Cage | Which Grows Faster?1. Floor systems provide broilers with direct access to littered floor areas
2. Automatic feeding systems distribute formulated feed through mechanical delivery lines
3. Nipple drinking systems provide controlled water access throughout production areas
4. Ventilation systems regulate air movement through mechanically controlled airflow
5. Reception /WhatsApp NO. : +8618830120193Read more Imported Vs Local Feed Mills | Which Offers Better Quality?1. Feed quality depends on coordinated processing stages
2. Grinding consistency influences subsequent mixing performance
3. Conditioning prepares mash for controlled pellet formation
4. Cooling stabilizes pellets before storage and handling
5. Reception /WhatsApp NO. : +8618830120193Read more 3 Key Differences Between H Type Chicken Cages And Traditional Layer Cages1. H Type cages arrange multiple tiers within poultry houses
2. Automatic systems coordinate feeding and manure removal operations
3. Egg conveyors transfer collected eggs toward centralized handling points
4. Environmental equipment regulates ventilation cooling and drinking conditions
5. Reception /WhatsApp NO. : +8618830120193Read more Floor Rearing Broiler Farming | 5 Essential Management Tips1. Floor-rearing houses require coordinated environmental and mechanical systems
2. Feed delivery depends on reliable conveying and distribution equipment
3. Water management requires stable hydraulic components and regular inspection
4. Ventilation performance depends on building geometry and equipment coordination
5. Reception /WhatsApp NO. : +8618830120193Read more Modern Poultry Equipment Vs Old Equipment | Which Is More Efficient?1. Modern poultry houses require coordinated mechanical systems for stable production
2. Feeding automation reduces repeated material handling during daily operations
3. Ventilation equipment manages airflow through controlled mechanical movement
4. Cooling systems support thermal management during elevated outdoor conditions
5. Reception /WhatsApp NO. : +8618830120193Read more Battery Cage For Layers For Sale | 5 Key Buying Factors1. Cage rows should align with house columns and service aisles
2. Feeding equipment requires coordinated drive and control positioning
3. Egg transfer routes should connect directly with collection areas
4. Manure discharge points should match waste-handling infrastructure
5. Reception /WhatsApp NO. : +8618830120193Read more 7 Practical Ways To Reduce Pellet Machine Downtime1. Pellet quality depends on formulation, moisture, particle distribution, die selection, and conditioning parameters
2. Machine loading varies according to feed characteristics and operating configuration
3. Maintenance records provide useful evidence for diagnosing recurring equipment conditions
4. Production-line capacity should be matched across upstream and downstream processing sections
5. Reception /WhatsApp NO. : +8618830120193Read more Galvanized Vs Stainless Steel Feed Mixers | Which Lasts Longer?1. Galvanized and stainless steels use different corrosion-protection mechanisms
2. Mixer durability depends on material, geometry, fabrication, loading, and maintenance
3. Batch capacity should correspond with daily feed consumption requirements
4. Drive selection must match mixer torque and operating speed
5. Reception /WhatsApp NO. : +8618830120193Read more Local Supplier Vs China Poultry Cage Factory Price: 5 Key Comparisons1. Poultry cage layouts require coordinated building dimensions and equipment interfaces
2. Automated systems require electrical planning before mechanical installation begins
3. Manure removal routes should align with cage row positions
4. Ventilation equipment requires airflow planning around house geometry
5. Reception /WhatsApp NO. : +8618830120193Read more Automatic Vs Semi-Automatic H Type Chicken Cages: Which To Choose?1. H type cages organize birds through vertical tiered housing structures
2. Automatic systems coordinate repetitive material handling across production areas
3. Semi-automatic systems retain manual steps for selected operations
4. Farm layouts determine equipment positioning, routing, and maintenance access
5. Reception /WhatsApp NO. : +8618830120193Read more How To Start A Small Poultry Farm Using An A Type Battery Cage? 5 Beginner Steps1. A Type cage layouts require coordinated building dimensions and equipment clearances
2. Feed distribution requires electrical and mechanical interfaces before installation
3. Ventilation capacity depends on building volume and local climate
4. Manure handling frequency varies with flock and environmental conditions
5. Reception /WhatsApp NO. : +8618830120193Read more Nipple Drinker System Efficiency | 6 Practical Optimization Tips1. Water lines should remain mechanically supported during daily operation
2. Pipeline routing should allow accessible inspection points for maintenance
3. Pressure regulation should follow the selected valve specification
4. Flushing assemblies should remain accessible after installation
5. Reception /WhatsApp NO. : +8618830120193Read more How To Upgrade Pralson Feeders | 5 Key Strategies1. Feeder alignment affects consistent feed movement across production lines
2. Pan positioning should follow bird development throughout each cycle
3. Suspension adjustment supports controlled equipment access during maintenance
4. System inspection records help identify mechanical deviations earlier
5. Reception /WhatsApp NO. : +8618830120193Read more Feed Mixer Vs Traditional Mixing | Which Improves Feed Quality?1. Feed quality depends on consistent ingredient preparation and handling
2. Particle-size testing provides measurable evidence for ration structure
3. Moisture conditions can influence laboratory particle distribution
4. Mixer settings require validation against individual ration characteristics
5. Reception /WhatsApp NO. : +8618830120193Read more A Type Vs H Type Poultry Cage Price: Which Is More Cost-Effective?1. A-type cages commonly use galvanized Q235 steel construction for commercial layer production
2. H-type systems provide vertical configurations for intensive poultry-house layouts
3. Automatic systems integrate feeding, drinking, egg collection, and manure handling
4. Project dimensions determine final equipment quantities and installation requirements
5. Reception /WhatsApp NO. : +8618830120193Read more H Type Battery Cages Vs Cage-Free Poultry Systems: Which Is More Profitable?1. H Type Battery Cages require precise engineering calculations for commercial farming applications
2. Professional poultry facilities integrate feeding and environmental management systems
3. Modern farms utilize automated equipment for stable production performance
4. Industrial layer operations depend on accurate equipment configuration planning
5. Reception /WhatsApp NO. : +8618830120193Read more What Certifications Are Required For An A Type Poultry Cage System? 4 Key Standards1. A Type Poultry Cage System uses structured engineering designs
2. Automatic Layer Cage System supports organized poultry production workflows
3. Poultry Cage Equipment integrates practical farm management requirements
4. Certified structures improve commercial farming planning efficiency
5. Reception /WhatsApp NO. : +8618830120193Read more 5 Proven Ways To Reduce Water Costs With Nipple Drinkers1. Nipple valves deliver water through controlled mechanical activation points
2. Pressure regulation supports consistent distribution across drinking lines
3. Filtration protects valve passages from suspended particulate matter
4. Suspension assemblies maintain drinking-line positioning during operation
5. Reception /WhatsApp NO. : +8618830120193Read more Hydraulic Vs Mechanical Pellet Machines | Which Is Safer?1. Feed conditioning depends on formulation, moisture, steam availability
2. Die selection considers ingredients, diameter, compression, and schedule
3. Cooling design considers temperature, moisture, ambient, storage needs
4. Equipment layout coordinates loading, access, routing, maintenance clearances
5. Reception /WhatsApp NO. : +8618830120193Read more High-Capacity Vs Small Feed Mills | Which Is More Profitable?1. Feed demand calculations connect flock population with daily ration requirements
2. Production scheduling determines equipment utilization and operating-hour allocation
3. Storage planning supports continuity between feed production and poultry-house consumption
4. Equipment integration reduces unnecessary transfer stages across production processes
5. Reception /WhatsApp NO. : +8618830120193Read more Manual Vs Automatic Poultry Cage System Cost: 6 Budget Comparisons1. Layer cage dimensions influence row planning and bird distribution
2. Feed systems determine material flow across production sections
3. Manure handling requires synchronized belt movement and discharge
4. Egg collection depends on conveyor alignment and transfer design
5. Reception /WhatsApp NO. : +8618830120193Read more H Type Chicken Cages Vs A Type Poultry Cages: Which Suits Large Farms Better?1. H Type Chicken Cages improve commercial poultry production efficiency through optimized structural systems
2. Automatic feeding integration supports stable farm operation with precise equipment coordination
3. Modern cage designs combine durable materials and practical management requirements
4. Large poultry facilities use engineered layouts for organized production environments
5. Reception /WhatsApp NO. : +8618830120193Read more How To Improve Hen Welfare In An A Type Layer Cage System? 5 Responsible Practices1. A Type Layer Cage System supports modern farms with reliable production structures
2. Professional cage solutions improve daily poultry management efficiency
3. Advanced equipment design supports sustainable egg production development
4. Technical engineering creates organized farming environments
5. Reception /WhatsApp NO. : +8618830120193Read more How To Raise Broilers Using Deep Litter System | 6 Practical Steps1. Deep litter floors require consistent bedding distribution across occupied house areas
2. Automatic drinking systems influence moisture management around water stations
3. Ventilation equipment removes accumulated heat, moisture, and airborne gases during production
4. Environmental controllers coordinate multiple poultry-house systems through sensor-based operating conditions
5. Reception /WhatsApp NO. : +8618830120193Read more How To Raise Broilers In Free Range System | 6 Practical Steps1. House dimensions determine equipment placement and service clearance requirements
2. Outdoor access requires secure boundaries and controlled movement
3. Ventilation design must account for local climate conditions
4. Equipment maintenance routes should remain accessible throughout operation
5. Reception /WhatsApp NO. : +8618830120193Read more How To Raise Broilers Using Floor Rearing System | 6 Practical Steps1. Floor systems require clean bedding before chick placement begins
2. Feeding lines should remain accessible for routine inspection
3. Water lines require regular flushing throughout production cycles
4. Equipment layouts should preserve maintenance access around motors
5. Reception /WhatsApp NO. : +8618830120193Read more Commercial Poultry Equipment Vs Small Farm Equipment | Which To Choose?1. Commercial houses require coordinated equipment layouts from the initial engineering stage
2. Small farms can prioritize modular systems with straightforward maintenance requirements
3. Future expansion should be considered before selecting permanent equipment interfaces
4. Climate conditions influence ventilation, cooling, and environmental-control configuration
5. Reception /WhatsApp NO. : +8618830120193Read more Single Feeder Vs Feeder Set | Which Works Best For Chicken Houses?1. Single feeders support compact feeding arrangements within smaller poultry buildings
2. Feeder sets coordinate multiple feeding points through centralized conveying
3. Automatic controls reduce repetitive manual feeding operations during production
4. House dimensions determine practical line quantity and equipment configuration
5. Reception /WhatsApp NO. : +8618830120193Read more Continuous Vs Batch Pellet Machines | Which Is More Efficient?1. Batch processing supports controlled recipe changes between production cycles
2. Feed storage capacity should match daily poultry consumption requirements
3. Automatic feeding circuits distribute finished pellets throughout chicken houses
4. Production planning should include maintenance and future expansion requirements
5. Reception /WhatsApp NO. : +8618830120193Read more Automatic Vs Manual Feed Mixers | Which Is More Efficient?1. Automatic feed mixing improves nutrient distribution across poultry production cycles
2. Feed mixer structures include shafts blades motors and control units
3. Equipment selection depends on farm capacity feed formula and operation goals
4. Maintenance planning supports stable machine performance during production periods
5. Reception /WhatsApp NO. : +8618830120193Read more




Search
Hot product
 IoT Poultry Farming System1. CO₂ 0–5,000 ppm range
2. NH₃ 0–100 ppm
3. RH ±3%
4. Thresholds in the 10–25 ppm range
5. Reception /WhatsApp NO. : +8618830120193Read more Overall Structure IoT System In The Farm1. Breeding planning framework
2. CCTV
3. Poultry digital platform - comprehensive large screen
4. Alarm management
5. Reception /WhatsApp NO. : +8618830120193Read more Poultry House Environmental Control Smart IoT System1. Precision ventilation
2. Full site equipment control
3. Self diagnosis alarm system
4. European standard hardware
5. Reception /WhatsApp NO. : +8618830120193Read more
Contact us
Phone(whatsapp No. ):
E-mail:
Office 1 (Hong Kong):
Flat/RM A, 15/F, ManlyCommercial Building 15 Soy Street, Mong Kok
Office 2 (China Mainland):
Flat/RM 2416, 24/F, Runxing Building, Youyi Nan Street, Shijiazhuang City, Hebei Province