


News
Pellet machine performance improvement requires systematic control of raw material properties, die specifications, conditioning parameters, maintenance schedules, and production monitoring systems.
Pellet mill efficiency is strongly influenced by particle size distribution, moisture consistency, compression ratio selection, and stable operating loads throughout continuous production cycles.
Advanced pellet production optimization practices can reduce electricity consumption, increase throughput capacity, improve pellet durability, and extend critical component service life.
Engineering-based process management enables manufacturers to achieve predictable product quality while minimizing downtime, maintenance expenses, and equipment wear.
Examines practical operating strategies, scientific principles, performance benchmarks, maintenance methods, and economic considerations for maximizing production results.
Get professional poultry farm construction guidance, equipment selection solutions, and the latest price lists, whatsApp to +8618830120193, click to learn more:
Why Pellet Machine Optimization Matters
Many factories focus on purchasing larger pellet mills but overlook daily optimization practices.
In reality, machine settings, material preparation, die condition, and operating procedures often have a greater impact on final production results than machine size alone.
Data is for reference only.Swipe horizontally to view full table.
Even modest improvements in these indicators can create substantial annual savings for medium and large production facilities.
Control Raw Material Particle Size
Raw material preparation is the first and most important factor affecting pellet machine performance.
Uniform particle size improves compression efficiency and ensures stable material flow through the die channels.
When particles are excessively large, the roller must exert greater force to push material through the die.
This increases mechanical stress and energy consumption.
Extremely fine particles may reduce throughput and increase dust generation.
Data is for reference only.Swipe horizontally to view full table.
Plants maintaining these particle size ranges often report smoother feeding characteristics and more stable pellet density.
Understanding Pellet Formation Science
Pellet production is fundamentally a thermomechanical process.
During compression, pressure and friction generate heat inside the die channels.
This heat changes the physical properties of starch, protein, lignin, and cellulose.
In feed production, starch gelatinization begins around 60°C and increases significantly between 70°C and 85°C.
The gelatinized starch acts as a natural binder, improving pellet strength.
For biomass pellets, lignin softens under elevated temperature and pressure.
Once cooled, the lignin solidifies and binds biomass fibers together without requiring external adhesives.
This scientific principle explains why temperature control, moisture management, and compression ratio directly influence pellet quality and pellet mill efficiency.
Maintain Proper Moisture Content
Moisture content has a direct impact on pellet density, durability, and machine productivity.
Insufficient moisture reduces material plasticity and increases friction inside die holes.
Excessive moisture can cause die blockage, pellet cracking, and cooling difficulties.
Data is for reference only.Swipe horizontally to view full table.
Maintaining moisture within these ranges helps achieve stable pellet formation while minimizing unnecessary power consumption.
Optimize Die Selection
The die is the most critical working component in any pellet machine.
Choosing the correct die specification can dramatically improve both production volume and pellet quality.
Many factories mistakenly use a single die configuration for all materials.
However, different materials require different compression characteristics.
Data is for reference only.Swipe horizontally to view full table.
A properly selected die reduces slippage between rollers and materials while improving pellet consistency.
Understanding Roller And Die Interaction
Inside the pellet chamber, rollers continuously force material against the rotating die surface.
The effectiveness of this interaction determines production efficiency.
When roller clearance becomes excessive, materials circulate within the chamber instead of entering die holes.
This lowers output and increases power consumption.
Industry maintenance records indicate that roller-to-die clearance between 0.10 mm and 0.30 mm generally provides stable compression performance for most feed pellet applications.
Routine adjustment prevents unnecessary wear while maintaining optimum throughput.
Improve Conditioning Efficiency
Conditioning introduces steam before pelleting.
This process increases material temperature, improves moisture distribution, and enhances binding characteristics.
Proper conditioning significantly reduces mechanical resistance during pelleting.
Data is for reference only.Swipe horizontally to view full table.
Plants utilizing effective conditioning systems often experience measurable reductions in machine load while achieving stronger pellets.
Establish Preventive Maintenance Programs
Preventive maintenance remains one of the most cost-effective optimization methods available.
Unexpected equipment failure frequently results in lost production hours, labor expenses, and emergency replacement costs.
Instead of waiting for failures, operators should follow planned inspection schedules based on operating hours.
Data is for reference only.Swipe horizontally to view full table.
Consistent maintenance improves machine reliability and protects expensive production assets.
Monitoring Key Production Indicators
Modern pellet plants increasingly rely on data-driven management systems.
Operators can identify performance losses before they become serious problems.
Important indicators include throughput, motor load, pellet temperature, energy usage, and finished product quality.
Data is for reference only.Swipe horizontally to view full table.
Tracking these indicators allows managers to make timely adjustments and maintain production consistency.
Energy Consumption Reduction Techniques
Electricity represents a major operating expense in pellet production facilities.
Even small reductions in energy usage can create significant annual savings.
Operators should focus on material preparation, conditioning efficiency, die maintenance, and motor performance.
Practical measures include maintaining sharp hammer mill screens, minimizing material recirculation, ensuring balanced roller pressure, and eliminating unnecessary idle operation.
A production line processing 50000 tons annually can save more than $18000 per year through systematic energy management.
European union standard reference only.
Common Operational Mistakes That Reduce Performance
Several common mistakes continue to affect pellet production optimization across many facilities.
Examples include operating with worn dies, feeding materials with inconsistent moisture levels, neglecting lubrication schedules, and increasing feed rates beyond machine design capacity.
Another frequent issue is attempting to compensate for poor pellet quality by increasing roller pressure.
While this may temporarily improve appearance, it often accelerates die wear and increases maintenance costs.
Long-term performance improvements are achieved through systematic process control rather than excessive mechanical force.
Advanced Automation For Pellet Machine Optimization
Automation technologies are becoming increasingly important in modern pellet manufacturing plants.
Variable-frequency drives, intelligent feeding systems, and automated lubrication equipment help maintain stable operating conditions.
Data is for reference only.Swipe horizontally to view full table.
These technologies provide measurable benefits and reduce dependence on manual adjustments.
Long-Term Economic Benefits
Optimization should be viewed as a long-term investment rather than a short-term operating adjustment.
A pellet machine operating at peak efficiency produces more saleable product, consumes less electricity, requires fewer spare parts, and experiences less downtime.
Over several years, these cumulative benefits often exceed the original cost of optimization programs, monitoring systems, and maintenance improvements.
Factories that continuously monitor performance indicators typically achieve greater production stability and stronger profitability compared with facilities relying solely on reactive maintenance strategies.
Frequently Asked Questions
Q1: What is the most important factor affecting pellet machine performance?
Raw material preparation is typically the most influential factor.
Uniform particle size, stable moisture content, and proper conditioning improve die utilization, pellet durability, and production capacity while reducing energy consumption.
Q2: How often should a pellet mill die be inspected?
Routine inspections should be performed according to operating hours and material characteristics.
Many facilities inspect die surfaces every 500 operating hours to identify wear patterns before production efficiency declines.
Q3: Can automation improve pellet mill efficiency?
Yes.
Automation systems provide accurate control of feeding rates, lubrication schedules, temperature monitoring, and moisture regulation.
Stable operating conditions help improve product consistency and reduce unexpected shutdowns.
Taiyu (HK) Group - One Of China Largest Pellet Machine Manufacturer
Professional pellet machines for feed pellets, biomass pellets, organic fertilizer pellets, and industrial granulation applications.
Global factory-direct supply with competitive pricing and stable manufacturing quality.
Complete poultry equipment and integrated production solutions for modern agricultural projects.
Professional Turn-key engineering services including design, manufacturing, installation, and commissioning.
Export experience covering multiple international markets with technical support and spare parts services.
Contact Us To Received Your Customized Poultry Farm Plan
Headquarters And Branchs
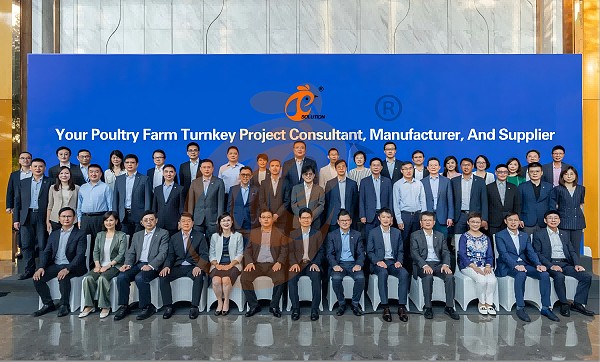
Hong Kong Headquarter Management Team
Hong Kong Headquarter Taiyu Industrial Group CO., LTD
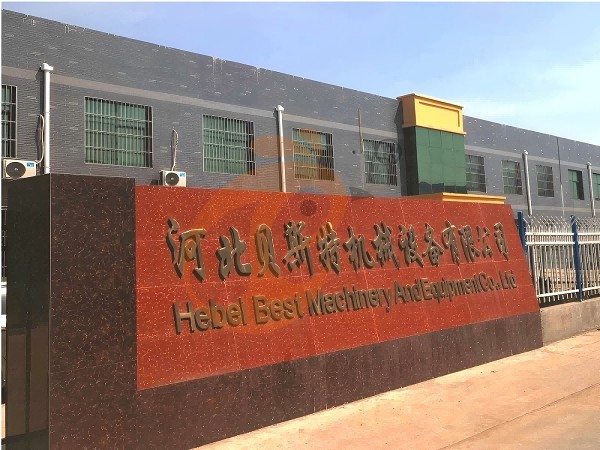
China Hebei Best Machinery And Equipment CO., LTD
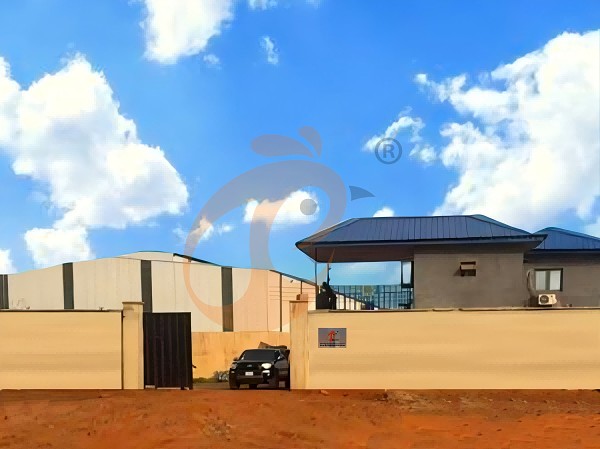
Nigeria Vanke Machinery And Equipment CO., LTD
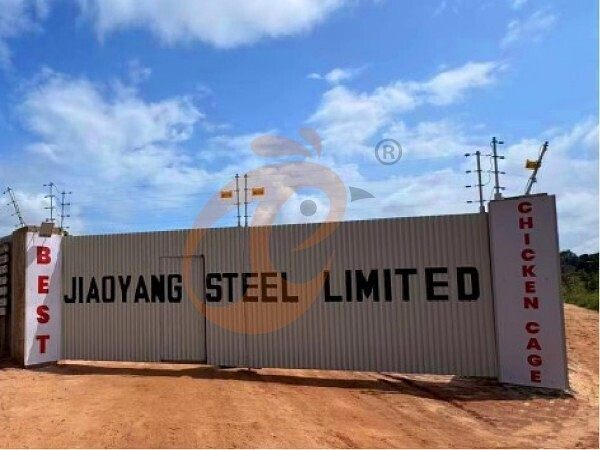
Tanzania Best Machinery And Equipment CO., LTD
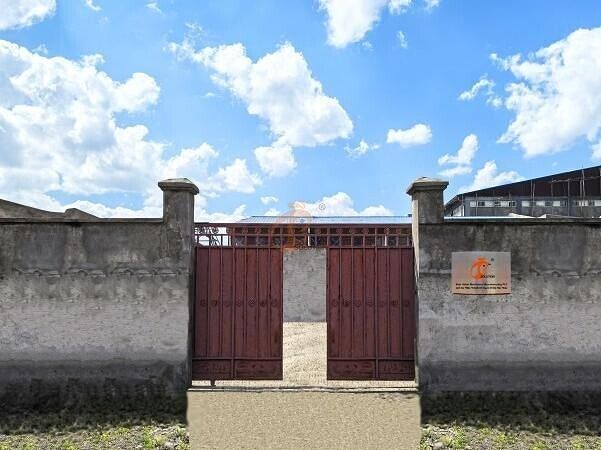
Ethiopia Best Hebei Machinery Manufacturing PLC
Reception /24 WhatsApp NO. : +8618830120193
FAQ
What Feeding System Standards Are Required For Pellet Machine In Poultry Chicken Feed Production Lines?
Feeder capacity is designed at 1.2–2.5 tons per hour depending on raw material density.
Flow consistency deviation is maintained within ±2% for uniform pellet quality output.
What Maintenance And Wear Part Replacement Standards Apply To Pellet Machine?
Bearing replacement intervals typically occur every 12–18 months under continuous operation.
Gearbox oil change frequency is maintained at 1000–1500 operating hours for system reliability.
What Safety Protection Systems Are Integrated In Pellet Machine For Poultry Chicken Feed Production?
Emergency stop response time is maintained within 0.5–1.0 seconds for operational safety.
Vibration monitoring limits are set at 4.5–6.0 mm/s to prevent mechanical failure.
Product Recommendations
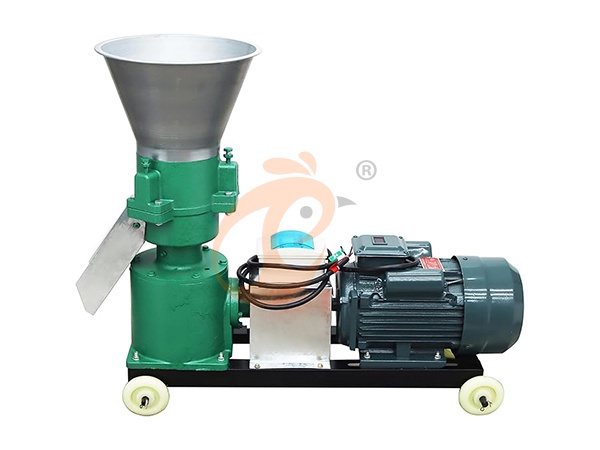
 Pellet Machine Lubrication | 6 Essential Steps For Longevity1. Regular lubrication helps maintain mechanical contact surfaces during repeated pellet production cycles
2. Cleaning procedures reduce contamination around critical moving components during servicing operations
3. Inspection records provide measurable evidence for maintenance decisions across production periods
4. Correct lubricant selection supports bearings, gear systems, shafts, and transmission assemblies
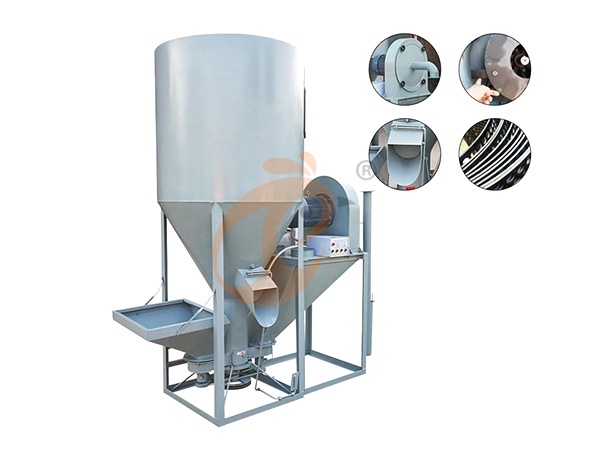
5. Reception /WhatsApp NO. : +8618830120193Read more Manual Feeding Vs Feed Mixer Automation | Which Costs Less?1. Feed mixer automation connects preparation and distribution stages
2. Mechanical mixing reduces repeated manual feed handling
3. Controlled conveying establishes a fixed material route
4. Automatic feeding supports scheduled delivery operations
5. Reception /WhatsApp NO. : +8618830120193Read more Poultry Cage Price For Africa Vs Asia Market: 4 Cost Differences1. Poultry cage layouts depend on flock capacity and house geometry
2. Equipment specifications should align with local operating conditions
3. Shipping calculations require verified packing dimensions and quantities
4. Commissioning procedures should cover mechanical and electrical systems
5. Reception /WhatsApp NO. : +8618830120193Read more H Type Chicken Cages Vs Flat House Poultry Systems: Which Saves Space?1. H Type Chicken Cages distribute birds across multiple vertical levels
2. Automatic feeding equipment follows dedicated cage-row routes
3. Manure removal equipment transfers waste toward collection points
4. Building dimensions determine final equipment arrangement and capacity
5. Reception /WhatsApp NO. : +8618830120193Read more How To Avoid Common Buying Mistakes When Choosing An A Type Poultry Cage? 5 Smart Tips1. Cage selection should follow building dimensions and flock requirements
2. Equipment interfaces require verification before manufacturing starts
3. Technical drawings help prevent installation conflicts and modifications
4. Automation modules can be selected according to operational priorities
5. Reception /WhatsApp NO. : +8618830120193Read more How To Improve Growth Rate In Broiler Floor Rearing System | 5 Tips1. Broiler houses require coordinated airflow, feeding, and drinking equipment
2. Environmental conditions influence bird comfort and production consistency
3. Automatic systems reduce repetitive manual management during daily operations
4. Equipment layout should follow flock capacity and house dimensions
5. Reception /WhatsApp NO. : +8618830120193Read more Poultry Farm Equipment Cost | 6 Key Factors Affecting Price And ROI1. Poultry farm equipment selection should match bird capacity and building dimensions
2. Automatic systems coordinate repetitive operations across multiple production areas
3. Ventilation equipment requires airflow calculations based on house conditions
4. Lifecycle costing should include maintenance, energy, and replacement requirements
5. Reception /WhatsApp NO. : +8618830120193Read more Hot-Dip Galvanized Vs Painted Battery Cage For Layers | Which Lasts Longer?1. Hot-dip galvanization creates zinc-based protection around prepared steel surfaces
2. Layer-house humidity and ammonia influence corrosion exposure during operation
3. Automatic feeding and manure systems require compatible cage-bank layouts
4. Maintenance planning remains important throughout commercial equipment service
5. Reception /WhatsApp NO. : +8618830120193Read more High Density Vs Low Density Broiler Chicken Cages | Which Performs Better?1. Multi-tier cage structures organize commercial broiler production vertically
2. Automatic feeding reduces repetitive manual feed distribution work
3. Ventilation design must match total building heat loads
4. Manure removal equipment supports cleaner production workflows
5. Reception /WhatsApp NO. : +8618830120193Read more How To Upgrade Old Water Lines To Nipple Drinkers | 5 Steps1. Drinking lines require systematic inspection before replacement work begins
2. Nipple positions should follow bird access and house geometry
3. Pressure checks verify proper operation across complete lines
4. Flushing removes installation debris before flock commissioning
5. Reception /WhatsApp NO. : +8618830120193Read more Floor Rearing System For Broilers Vs Cage | Which Grows Faster?1. Floor systems provide broilers with direct access to littered floor areas
2. Automatic feeding systems distribute formulated feed through mechanical delivery lines
3. Nipple drinking systems provide controlled water access throughout production areas
4. Ventilation systems regulate air movement through mechanically controlled airflow
5. Reception /WhatsApp NO. : +8618830120193Read more Imported Vs Local Feed Mills | Which Offers Better Quality?1. Feed quality depends on coordinated processing stages
2. Grinding consistency influences subsequent mixing performance
3. Conditioning prepares mash for controlled pellet formation
4. Cooling stabilizes pellets before storage and handling
5. Reception /WhatsApp NO. : +8618830120193Read more 3 Key Differences Between H Type Chicken Cages And Traditional Layer Cages1. H Type cages arrange multiple tiers within poultry houses
2. Automatic systems coordinate feeding and manure removal operations
3. Egg conveyors transfer collected eggs toward centralized handling points
4. Environmental equipment regulates ventilation cooling and drinking conditions
5. Reception /WhatsApp NO. : +8618830120193Read more Floor Rearing Broiler Farming | 5 Essential Management Tips1. Floor-rearing houses require coordinated environmental and mechanical systems
2. Feed delivery depends on reliable conveying and distribution equipment
3. Water management requires stable hydraulic components and regular inspection
4. Ventilation performance depends on building geometry and equipment coordination
5. Reception /WhatsApp NO. : +8618830120193Read more Modern Poultry Equipment Vs Old Equipment | Which Is More Efficient?1. Modern poultry houses require coordinated mechanical systems for stable production
2. Feeding automation reduces repeated material handling during daily operations
3. Ventilation equipment manages airflow through controlled mechanical movement
4. Cooling systems support thermal management during elevated outdoor conditions
5. Reception /WhatsApp NO. : +8618830120193Read more Battery Cage For Layers For Sale | 5 Key Buying Factors1. Cage rows should align with house columns and service aisles
2. Feeding equipment requires coordinated drive and control positioning
3. Egg transfer routes should connect directly with collection areas
4. Manure discharge points should match waste-handling infrastructure
5. Reception /WhatsApp NO. : +8618830120193Read more 7 Practical Ways To Reduce Pellet Machine Downtime1. Pellet quality depends on formulation, moisture, particle distribution, die selection, and conditioning parameters
2. Machine loading varies according to feed characteristics and operating configuration
3. Maintenance records provide useful evidence for diagnosing recurring equipment conditions
4. Production-line capacity should be matched across upstream and downstream processing sections
5. Reception /WhatsApp NO. : +8618830120193Read more Galvanized Vs Stainless Steel Feed Mixers | Which Lasts Longer?1. Galvanized and stainless steels use different corrosion-protection mechanisms
2. Mixer durability depends on material, geometry, fabrication, loading, and maintenance
3. Batch capacity should correspond with daily feed consumption requirements
4. Drive selection must match mixer torque and operating speed
5. Reception /WhatsApp NO. : +8618830120193Read more Local Supplier Vs China Poultry Cage Factory Price: 5 Key Comparisons1. Poultry cage layouts require coordinated building dimensions and equipment interfaces
2. Automated systems require electrical planning before mechanical installation begins
3. Manure removal routes should align with cage row positions
4. Ventilation equipment requires airflow planning around house geometry
5. Reception /WhatsApp NO. : +8618830120193Read more Automatic Vs Semi-Automatic H Type Chicken Cages: Which To Choose?1. H type cages organize birds through vertical tiered housing structures
2. Automatic systems coordinate repetitive material handling across production areas
3. Semi-automatic systems retain manual steps for selected operations
4. Farm layouts determine equipment positioning, routing, and maintenance access
5. Reception /WhatsApp NO. : +8618830120193Read more How To Start A Small Poultry Farm Using An A Type Battery Cage? 5 Beginner Steps1. A Type cage layouts require coordinated building dimensions and equipment clearances
2. Feed distribution requires electrical and mechanical interfaces before installation
3. Ventilation capacity depends on building volume and local climate
4. Manure handling frequency varies with flock and environmental conditions
5. Reception /WhatsApp NO. : +8618830120193Read more Nipple Drinker System Efficiency | 6 Practical Optimization Tips1. Water lines should remain mechanically supported during daily operation
2. Pipeline routing should allow accessible inspection points for maintenance
3. Pressure regulation should follow the selected valve specification
4. Flushing assemblies should remain accessible after installation
5. Reception /WhatsApp NO. : +8618830120193Read more How To Upgrade Pralson Feeders | 5 Key Strategies1. Feeder alignment affects consistent feed movement across production lines
2. Pan positioning should follow bird development throughout each cycle
3. Suspension adjustment supports controlled equipment access during maintenance
4. System inspection records help identify mechanical deviations earlier
5. Reception /WhatsApp NO. : +8618830120193Read more Feed Mixer Vs Traditional Mixing | Which Improves Feed Quality?1. Feed quality depends on consistent ingredient preparation and handling
2. Particle-size testing provides measurable evidence for ration structure
3. Moisture conditions can influence laboratory particle distribution
4. Mixer settings require validation against individual ration characteristics
5. Reception /WhatsApp NO. : +8618830120193Read more A Type Vs H Type Poultry Cage Price: Which Is More Cost-Effective?1. A-type cages commonly use galvanized Q235 steel construction for commercial layer production
2. H-type systems provide vertical configurations for intensive poultry-house layouts
3. Automatic systems integrate feeding, drinking, egg collection, and manure handling
4. Project dimensions determine final equipment quantities and installation requirements
5. Reception /WhatsApp NO. : +8618830120193Read more H Type Battery Cages Vs Cage-Free Poultry Systems: Which Is More Profitable?1. H Type Battery Cages require precise engineering calculations for commercial farming applications
2. Professional poultry facilities integrate feeding and environmental management systems
3. Modern farms utilize automated equipment for stable production performance
4. Industrial layer operations depend on accurate equipment configuration planning
5. Reception /WhatsApp NO. : +8618830120193Read more What Certifications Are Required For An A Type Poultry Cage System? 4 Key Standards1. A Type Poultry Cage System uses structured engineering designs
2. Automatic Layer Cage System supports organized poultry production workflows
3. Poultry Cage Equipment integrates practical farm management requirements
4. Certified structures improve commercial farming planning efficiency
5. Reception /WhatsApp NO. : +8618830120193Read more 5 Proven Ways To Reduce Water Costs With Nipple Drinkers1. Nipple valves deliver water through controlled mechanical activation points
2. Pressure regulation supports consistent distribution across drinking lines
3. Filtration protects valve passages from suspended particulate matter
4. Suspension assemblies maintain drinking-line positioning during operation
5. Reception /WhatsApp NO. : +8618830120193Read more Hydraulic Vs Mechanical Pellet Machines | Which Is Safer?1. Feed conditioning depends on formulation, moisture, steam availability
2. Die selection considers ingredients, diameter, compression, and schedule
3. Cooling design considers temperature, moisture, ambient, storage needs
4. Equipment layout coordinates loading, access, routing, maintenance clearances
5. Reception /WhatsApp NO. : +8618830120193Read more High-Capacity Vs Small Feed Mills | Which Is More Profitable?1. Feed demand calculations connect flock population with daily ration requirements
2. Production scheduling determines equipment utilization and operating-hour allocation
3. Storage planning supports continuity between feed production and poultry-house consumption
4. Equipment integration reduces unnecessary transfer stages across production processes
5. Reception /WhatsApp NO. : +8618830120193Read more Manual Vs Automatic Poultry Cage System Cost: 6 Budget Comparisons1. Layer cage dimensions influence row planning and bird distribution
2. Feed systems determine material flow across production sections
3. Manure handling requires synchronized belt movement and discharge
4. Egg collection depends on conveyor alignment and transfer design
5. Reception /WhatsApp NO. : +8618830120193Read more H Type Chicken Cages Vs A Type Poultry Cages: Which Suits Large Farms Better?1. H Type Chicken Cages improve commercial poultry production efficiency through optimized structural systems
2. Automatic feeding integration supports stable farm operation with precise equipment coordination
3. Modern cage designs combine durable materials and practical management requirements
4. Large poultry facilities use engineered layouts for organized production environments
5. Reception /WhatsApp NO. : +8618830120193Read more How To Improve Hen Welfare In An A Type Layer Cage System? 5 Responsible Practices1. A Type Layer Cage System supports modern farms with reliable production structures
2. Professional cage solutions improve daily poultry management efficiency
3. Advanced equipment design supports sustainable egg production development
4. Technical engineering creates organized farming environments
5. Reception /WhatsApp NO. : +8618830120193Read more How To Raise Broilers Using Deep Litter System | 6 Practical Steps1. Deep litter floors require consistent bedding distribution across occupied house areas
2. Automatic drinking systems influence moisture management around water stations
3. Ventilation equipment removes accumulated heat, moisture, and airborne gases during production
4. Environmental controllers coordinate multiple poultry-house systems through sensor-based operating conditions
5. Reception /WhatsApp NO. : +8618830120193Read more How To Raise Broilers In Free Range System | 6 Practical Steps1. House dimensions determine equipment placement and service clearance requirements
2. Outdoor access requires secure boundaries and controlled movement
3. Ventilation design must account for local climate conditions
4. Equipment maintenance routes should remain accessible throughout operation
5. Reception /WhatsApp NO. : +8618830120193Read more How To Raise Broilers Using Floor Rearing System | 6 Practical Steps1. Floor systems require clean bedding before chick placement begins
2. Feeding lines should remain accessible for routine inspection
3. Water lines require regular flushing throughout production cycles
4. Equipment layouts should preserve maintenance access around motors
5. Reception /WhatsApp NO. : +8618830120193Read more Commercial Poultry Equipment Vs Small Farm Equipment | Which To Choose?1. Commercial houses require coordinated equipment layouts from the initial engineering stage
2. Small farms can prioritize modular systems with straightforward maintenance requirements
3. Future expansion should be considered before selecting permanent equipment interfaces
4. Climate conditions influence ventilation, cooling, and environmental-control configuration
5. Reception /WhatsApp NO. : +8618830120193Read more Single Feeder Vs Feeder Set | Which Works Best For Chicken Houses?1. Single feeders support compact feeding arrangements within smaller poultry buildings
2. Feeder sets coordinate multiple feeding points through centralized conveying
3. Automatic controls reduce repetitive manual feeding operations during production
4. House dimensions determine practical line quantity and equipment configuration
5. Reception /WhatsApp NO. : +8618830120193Read more Continuous Vs Batch Pellet Machines | Which Is More Efficient?1. Batch processing supports controlled recipe changes between production cycles
2. Feed storage capacity should match daily poultry consumption requirements
3. Automatic feeding circuits distribute finished pellets throughout chicken houses
4. Production planning should include maintenance and future expansion requirements
5. Reception /WhatsApp NO. : +8618830120193Read more Automatic Vs Manual Feed Mixers | Which Is More Efficient?1. Automatic feed mixing improves nutrient distribution across poultry production cycles
2. Feed mixer structures include shafts blades motors and control units
3. Equipment selection depends on farm capacity feed formula and operation goals
4. Maintenance planning supports stable machine performance during production periods
5. Reception /WhatsApp NO. : +8618830120193Read more




Search
Hot product
 IoT Poultry Farming System1. CO₂ 0–5,000 ppm range
2. NH₃ 0–100 ppm
3. RH ±3%
4. Thresholds in the 10–25 ppm range
5. Reception /WhatsApp NO. : +8618830120193Read more Overall Structure IoT System In The Farm1. Breeding planning framework
2. CCTV
3. Poultry digital platform - comprehensive large screen
4. Alarm management
5. Reception /WhatsApp NO. : +8618830120193Read more Poultry House Environmental Control Smart IoT System1. Precision ventilation
2. Full site equipment control
3. Self diagnosis alarm system
4. European standard hardware
5. Reception /WhatsApp NO. : +8618830120193Read more
Contact us
Phone(whatsapp No. ):
E-mail:
Office 1 (Hong Kong):
Flat/RM A, 15/F, ManlyCommercial Building 15 Soy Street, Mong Kok
Office 2 (China Mainland):
Flat/RM 2416, 24/F, Runxing Building, Youyi Nan Street, Shijiazhuang City, Hebei Province